DL SHAH AWARD QUALITY COUNCIL OF INDIA QUALITY
- Slides: 39
DL SHAH AWARD QUALITY COUNCIL OF INDIA QUALITY IMPROVEMENT & STANDARDIZATION IN THE LINE CARTON PACKAGING CATEGORY – SPICES DHARAMPAL SATYAPAL GROUP DS SPICECO PVT LTD B-19, SECTOR – 3, NOIDA, U. P. INDIA 1
Contents Customer and Quality Focus Diagnostic Approach Methodology for Deployment Implementation of 7 QC Tools QC Team Effort Financial Benefits Derived Sustainability and Acceptability 2
CUSTOMER AND QUALITY FOCUS 3
CUSTOMER/ STAKEHOLDER SATISFACTION v Improved Quality v Improved Productivity v On-time Delivery v Optimum Utilization of Resources Social benefits • Energy Conservation • Optimum Utilisation of Resources/ Inputs – RM, PM etc. • Indirect Benefit – Reduction in the Cost of Production 4
DIAGNOSTIC APPROACH 5
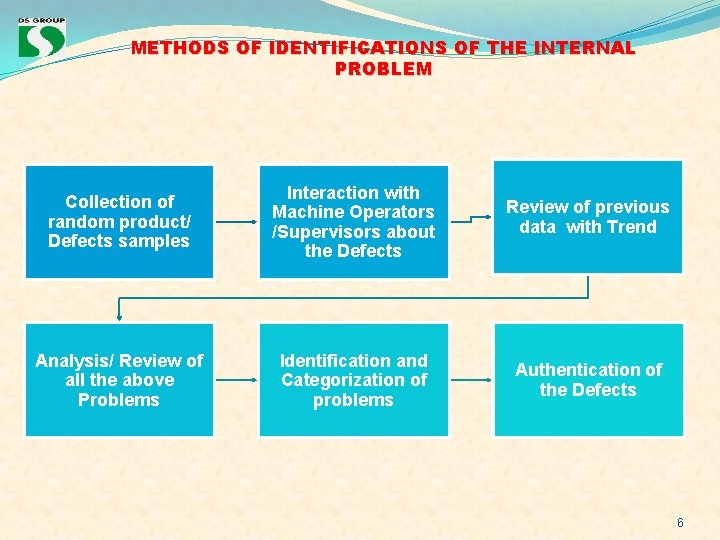
METHODS OF IDENTIFICATIONS OF THE INTERNAL PROBLEM Collection of random product/ Defects samples Interaction with Machine Operators /Supervisors about the Defects Review of previous data with Trend Analysis/ Review of all the above Problems Identification and Categorization of problems Authentication of the Defects 6
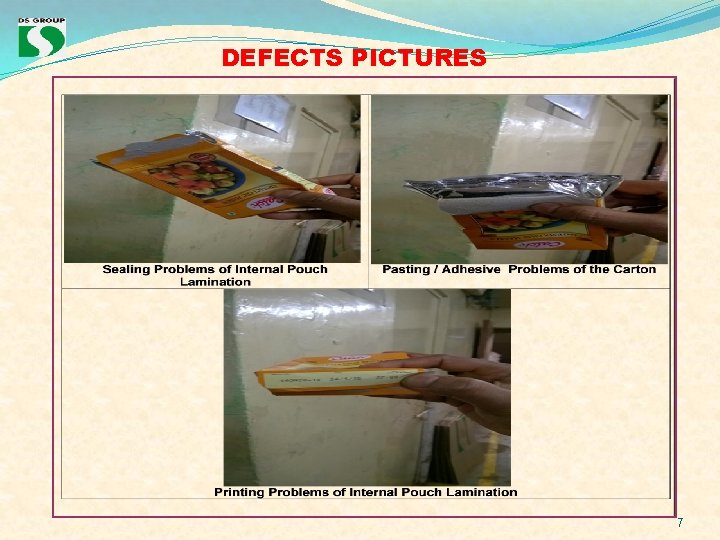
DEFECTS PICTURES 7
METHODOLOGY FOR DEPLOYMENT 8
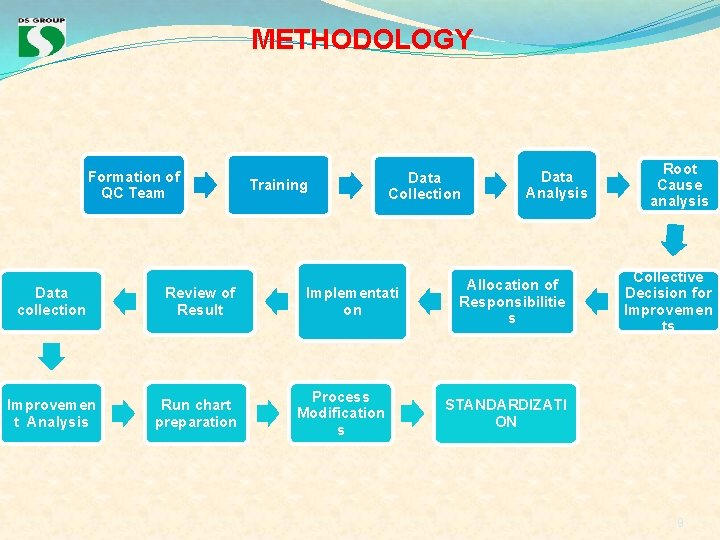
METHODOLOGY Formation of QC Team Data collection Review of Result Improvemen t Analysis Run chart preparation Training Data Collection Implementati on Process Modification s Data Analysis Allocation of Responsibilitie s Root Cause analysis Collective Decision for Improvemen ts STANDARDIZATI ON 9
IMPLEMENTATION OF 7 QC TOOLS TO SOLVE THE QUALITY PROBLEMS 10
QC TEAM Name of the Team – ISHIKAWA No. of Team Members – 4 Team Leader Team Member 1 Team Member 2 Team Member 3 11
DEGREE OF EFFORTS EMPLOYED ØFormation of Quality Circle ØIdentification of problems ØAllocation of Responsibilities ØMonitoring and study of collected samples ØReview and analysis of data ØCategorization of defects ØRoot Cause Analysis ØCorrective Action ØImplementation and follow up with the result ØFinal Review of the Output 12
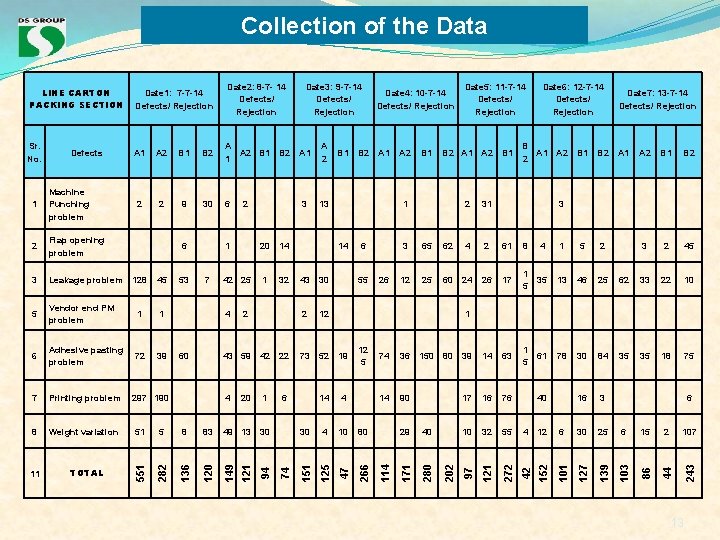
Collection of the Data Date 2: 8 -7 - 14 Defects/ Rejection LINE CARTON PACKING SECTION Date 1: 7 -7 -14 Defects/ Rejection Sr. No. A 1 A 2 B 1 B 2 A A 2 B 1 B 2 1 Machine Punching problem 2 2 9 30 6 2 3 13 1 2 31 3 2 Flap opening problem 6 1 20 14 6 3 65 62 4 2 61 8 4 1 5 2 3 2 45 3 Leakage problem 128 45 53 7 42 25 1 32 43 30 55 26 12 25 60 24 26 17 1 5 35 13 46 25 62 33 22 10 5 Vendor end PM problem 1 1 4 2 12 1 6 Adhesive pasting problem 72 39 60 43 59 42 22 73 52 19 12 5 74 36 39 14 63 1 5 61 78 30 84 35 35 18 75 7 Printing problem 297 190 4 20 1 6 14 4 14 90 17 16 76 40 16 3 6 8 Weight variation 51 5 8 83 49 13 30 30 4 10 80 29 40 10 32 55 4 12 6 30 25 6 15 2 107 121 272 42 152 101 127 139 103 86 44 TOTAL 121 11 2 150 80 243 1 97 B 2 202 B 1 280 A 2 171 A 1 114 B 2 266 B 1 47 B A 1 A 2 2 125 B 1 151 B 2 A 1 A 2 74 B 1 94 A 2 149 A 1 Date 7: 13 -7 -14 Defects/ Rejection 120 B 1 B 2 Date 6: 12 -7 -14 Defects/ Rejection 136 A 2 Date 5: 11 -7 -14 Defects/ Rejection 282 A 1 Date 4: 10 -7 -14 Defects/ Rejection 551 Defects Date 3: 9 -7 -14 Defects/ Rejection 13
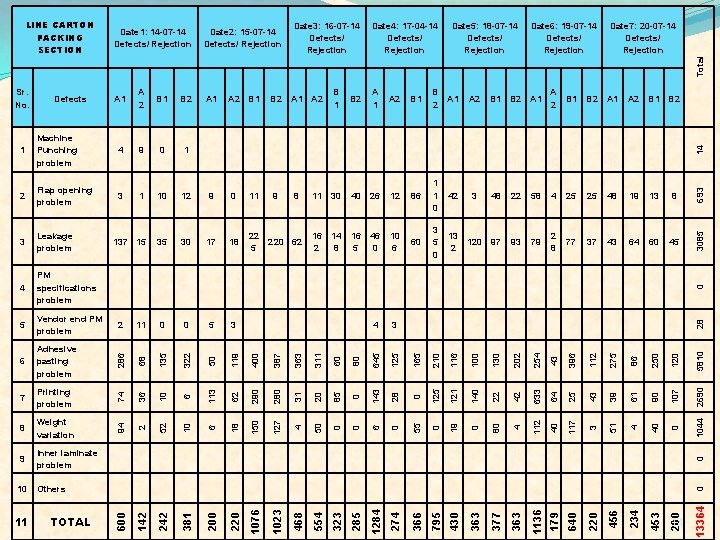
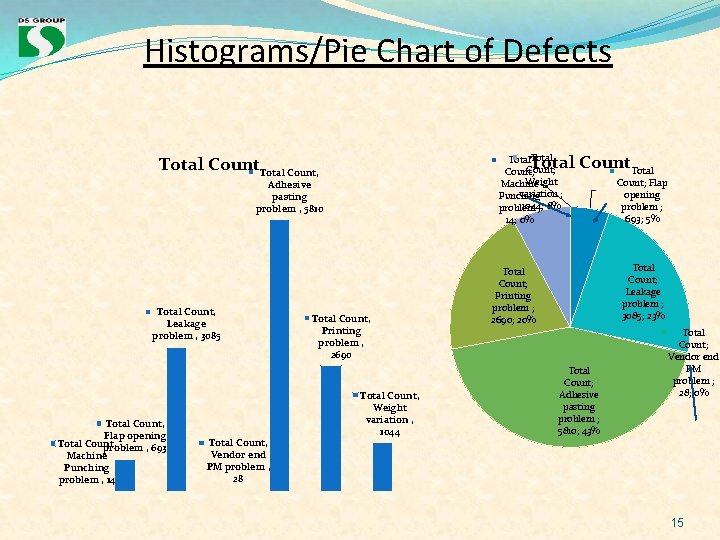
Date 1: 14 -07 -14 Defects/ Rejection Date 2: 15 -07 -14 Defects/ Rejection Date 3: 16 -07 -14 Defects/ Rejection A 1 A 2 Date 4: 17 -04 -14 Defects/ Rejection Date 5: 18 -07 -14 Defects/ Rejection Date 6: 19 -07 -14 Defects/ Rejection Date 7: 20 -07 -14 Defects/ Rejection Total LINE CARTON PACKING SECTION 2 Flap opening problem 3 1 10 12 9 0 11 9 8 11 30 40 26 12 86 1 1 0 42 3 48 22 58 4 25 25 48 19 13 8 3 Leakage problem 137 15 35 30 17 18 22 5 220 62 16 2 14 8 16 5 46 0 10 6 60 3 5 0 13 120 97 2 93 79 2 8 77 37 43 64 60 45 4 PM specifications problem 5 Vendor end PM problem 2 11 0 0 5 3 4 3 6 Adhesive pasting problem 7 Printing problem 280 31 20 85 0 143 28 0 125 121 140 22 42 633 64 25 43 39 61 90 107 8 Weight variation 127 4 50 0 0 6 0 55 0 19 0 80 4 112 40 117 3 51 4 40 0 9 Inner laminate problem 10 Others 0 468 554 323 285 1284 274 366 795 430 363 377 363 1136 179 640 220 456 234 453 280 13364 11 TOTAL 14 0 1044 2690 5810 28 0 3085 693 14 120 250 86 275 112 396 43 254 202 130 100 116 210 165 125 645 80 60 311 363 387 400 119 1 50 0 322 9 135 4 68 Machine Punching problem 286 1 1023 B 1 B 2 290 A 2 150 B 1 B 2 A 1 1076 A 2 62 B 1 B 2 A 1 18 A 2 220 A 1 113 B 2 6 B 1 200 A 2 6 A 1 10 B 2 381 B 1 10 B 2 52 A 2 B 1 242 A 1 36 B 2 2 B 1 142 A 2 74 A 1 94 Defects 600 Sr. No.
Histograms/Pie Chart of Defects Total Count; Weight Machine variation ; Punching 1044; problem ; 8% 14; 0% Total Count, Adhesive pasting problem , 5810 Total Count, Leakage problem , 3085 Total Count, Flap opening Total Count, problem , 693 Machine Punching problem , 14 Total Count, Vendor end PM problem , 28 Total Count, Printing problem , 2690 Total Count, Weight variation , 1044 Count; Flap opening problem ; 693; 5% Total Count; Leakage problem ; 3085; 23% Total Count; Printing problem ; 2690; 20% Total Count; Adhesive pasting problem ; 5810; 43% Total Count; Vendor end PM problem ; 28; 0% 15
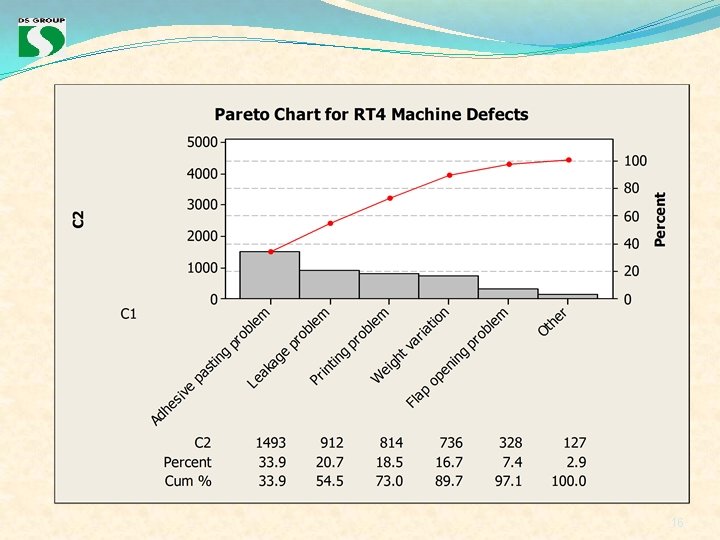
16
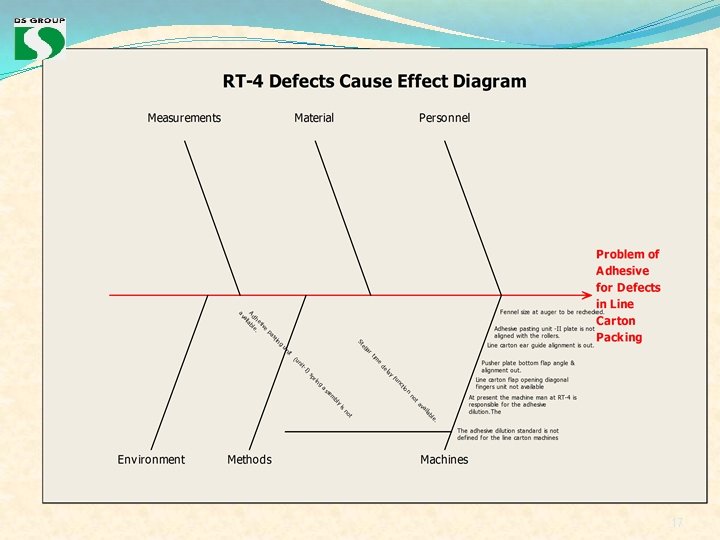
17
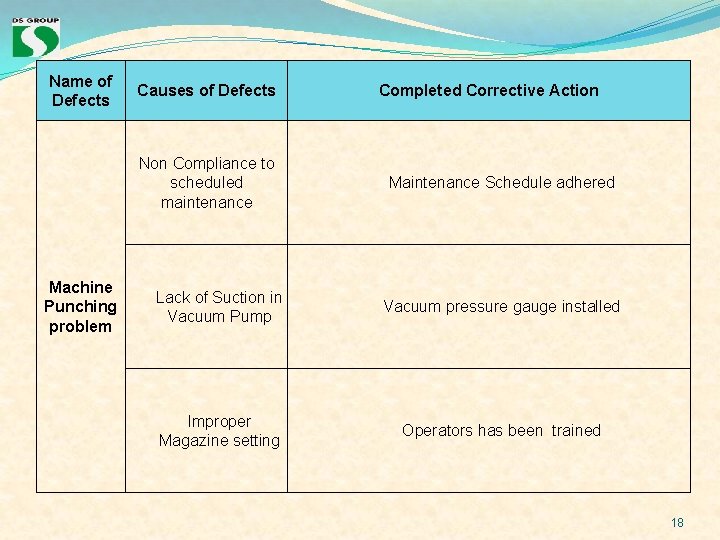
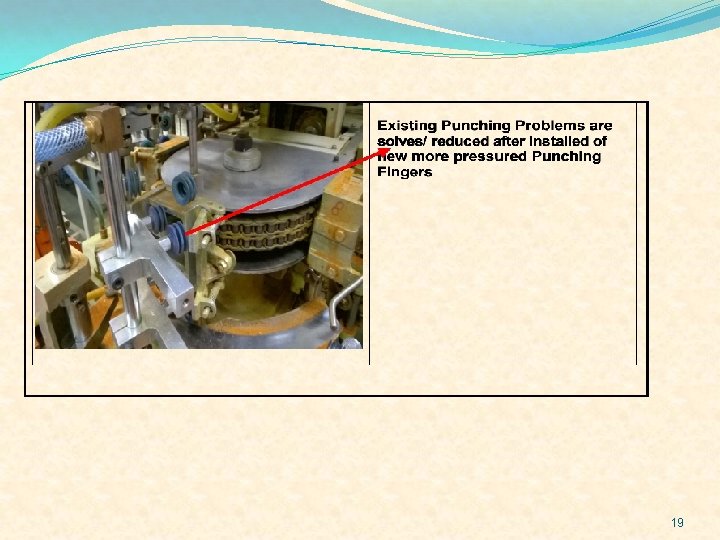
Name of Defects Causes of Defects Non Compliance to scheduled maintenance Machine Punching problem Completed Corrective Action Maintenance Schedule adhered Lack of Suction in Vacuum Pump Vacuum pressure gauge installed Improper Magazine setting Operators has been trained 18
19
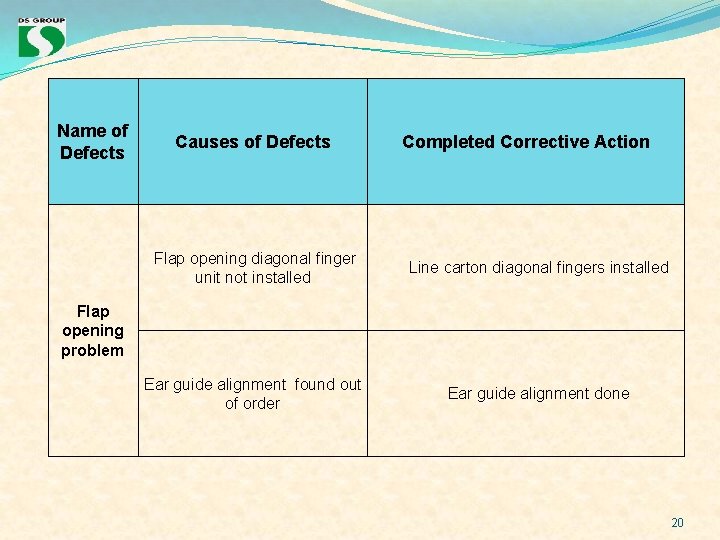
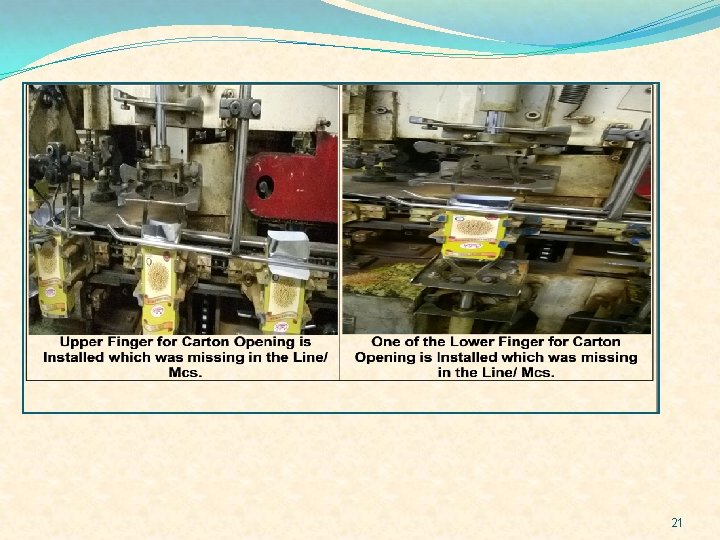
Name of Defects Causes of Defects Completed Corrective Action Flap opening diagonal finger unit not installed Line carton diagonal fingers installed Ear guide alignment found out of order Ear guide alignment done Flap opening problem 20
21
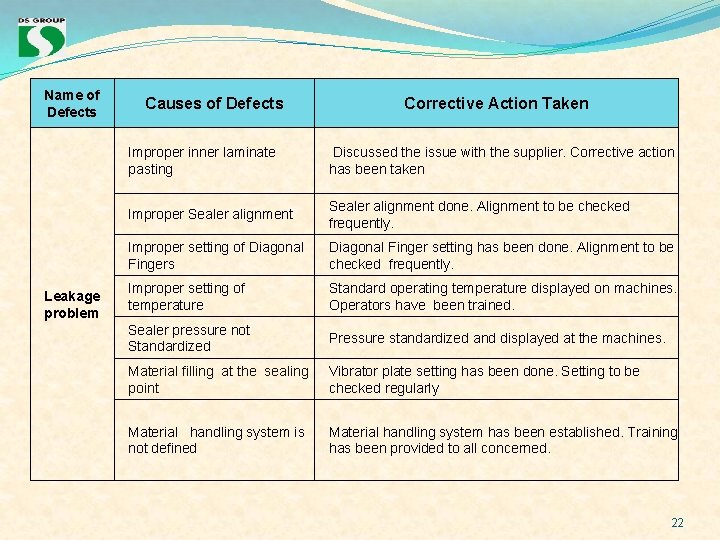
Name of Defects Leakage problem Causes of Defects Corrective Action Taken Improper inner laminate pasting Discussed the issue with the supplier. Corrective action has been taken Improper Sealer alignment done. Alignment to be checked frequently. Improper setting of Diagonal Fingers Diagonal Finger setting has been done. Alignment to be checked frequently. Improper setting of temperature Standard operating temperature displayed on machines. Operators have been trained. Sealer pressure not Standardized Pressure standardized and displayed at the machines. Material filling at the sealing point Vibrator plate setting has been done. Setting to be checked regularly Material handling system is not defined Material handling system has been established. Training has been provided to all concerned. 22
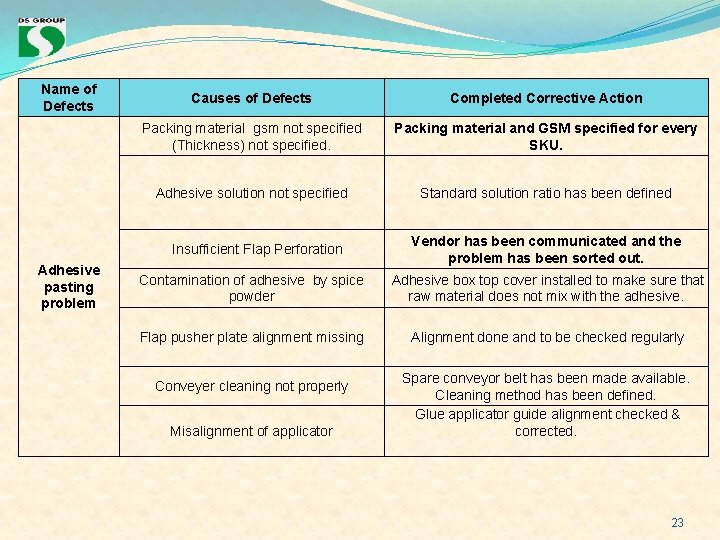
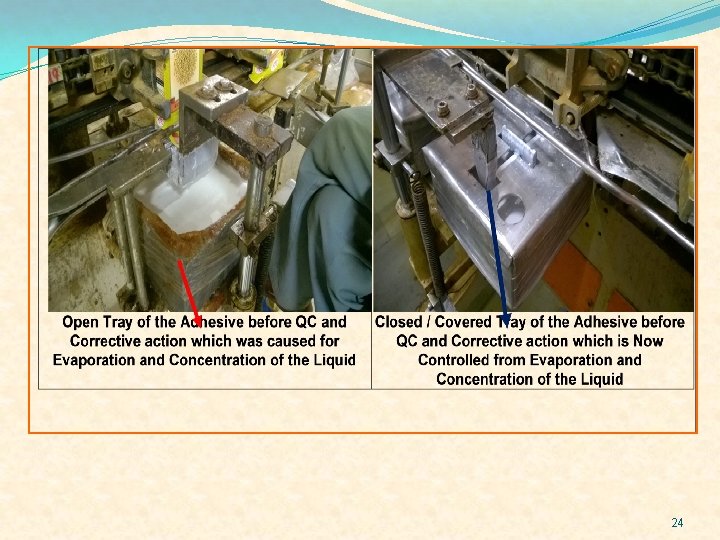
Name of Defects Adhesive pasting problem Causes of Defects Completed Corrective Action Packing material gsm not specified (Thickness) not specified. Packing material and GSM specified for every SKU. Adhesive solution not specified Standard solution ratio has been defined Insufficient Flap Perforation Vendor has been communicated and the problem has been sorted out. Contamination of adhesive by spice powder Adhesive box top cover installed to make sure that raw material does not mix with the adhesive. Flap pusher plate alignment missing Alignment done and to be checked regularly Conveyer cleaning not properly Misalignment of applicator Spare conveyor belt has been made available. Cleaning method has been defined. Glue applicator guide alignment checked & corrected. 23
24
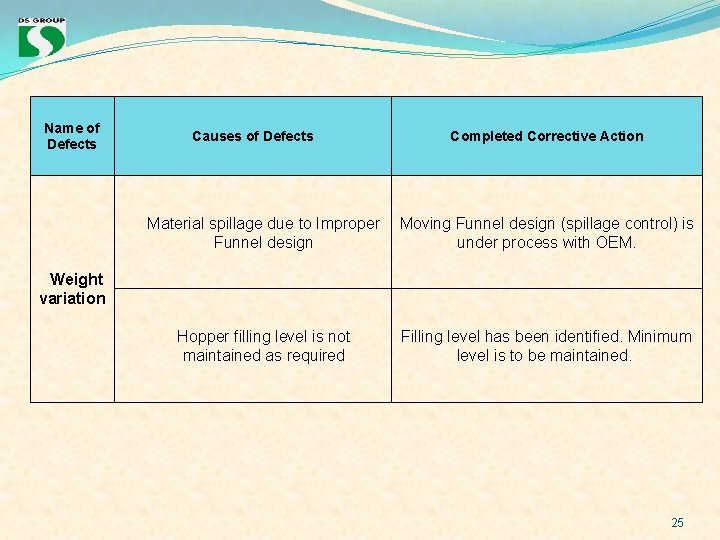
Name of Defects Causes of Defects Completed Corrective Action Material spillage due to Improper Moving Funnel design (spillage control) is Funnel design under process with OEM. Weight variation Hopper filling level is not maintained as required Filling level has been identified. Minimum level is to be maintained. 25
QC TEAM EFFORT 26
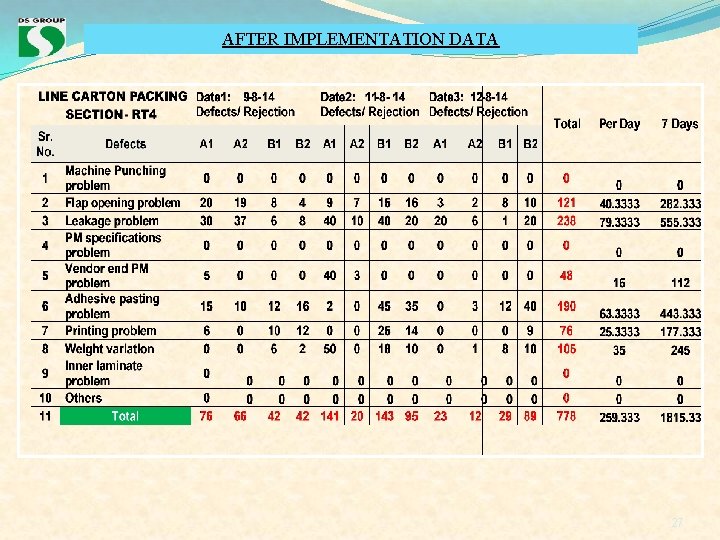
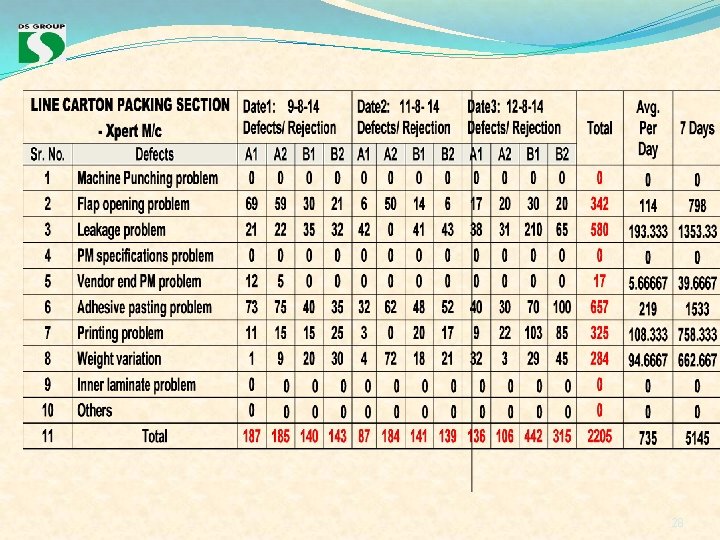
AFTER IMPLEMENTATION DATA 27
28
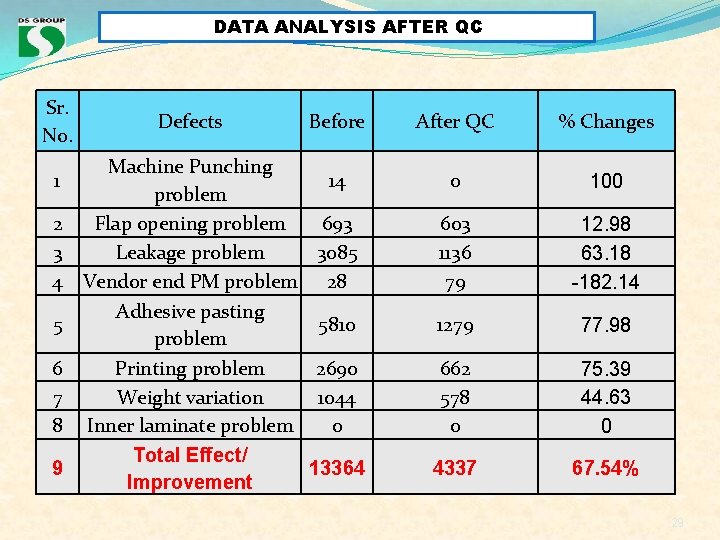
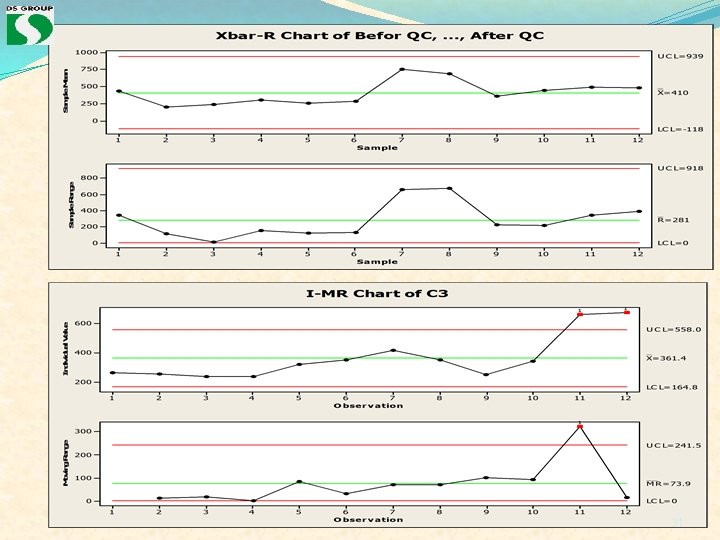
DATA ANALYSIS AFTER QC Sr. No. 1 2 3 4 5 6 7 8 9 Defects Before Machine Punching 14 problem Flap opening problem 693 Leakage problem 3085 Vendor end PM problem 28 Adhesive pasting 5810 problem Printing problem 2690 Weight variation 1044 Inner laminate problem 0 Total Effect/ 13364 Improvement After QC % Changes 0 100 603 1136 79 12. 98 63. 18 -182. 14 1279 77. 98 662 578 0 75. 39 44. 63 0 4337 67. 54% 29
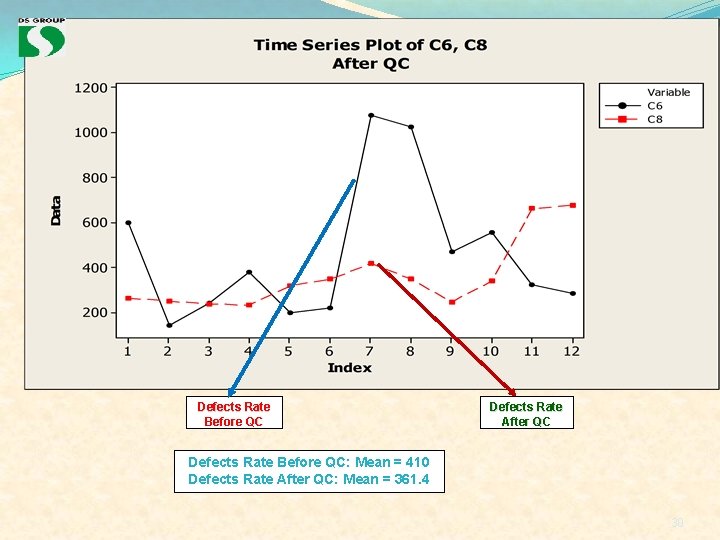
Defects Rate Before QC Defects Rate After QC Defects Rate Before QC: Mean = 410 Defects Rate After QC: Mean = 361. 4 30
31
FINANCIAL BENEFITS DERIVED 32
FINANCIAL AND TANGIBLE BENEFITS After the Implementation of the 7 QC tools for Quality Improvement with Internal Why analysis, the following Financial benefits are accrued by the Plant FINANCIAL AND TANGIBLE BENEFITS Following Financial benefits are accrued by the Plant. 1) Saving of in Reproduction / Reprocessing Cost of 2. 1% Rejected Materials of the Total Production 2. Reduction in the Cost of other Complementary Cost of the Production and Improve in Productivity – Manpower, Energy and Other Variable costs of the Production – Direct and Indirect 33
KNOWLEDGE CREATION 1. REDUCTION IN PRODUCT CHANGEOVER/ MACHINE STOPPAGE TIME Analysis results the following outcomes: Ø Ø Machine utilization against products Machine utilization against packing materials used Product selection against machine performance The above improves the utilization and stability of the machines. 2. RE-DESIGN OF THE PACKING MATERIAL QC on Packing Materials is in vogue in the System with the following areas; Ø Re-assess the Packing Materials with the Target of reducing Opening Problems Ø Reduction in the Quantity of the PM as per the M/c specification. Ø Reduction of Leakage problems in the finished products Ø Reduction in cost of the Packing Materials 3. REDUCTION IN THE PRE-PRINTED MATERIAL INVENTORY Ø Converted the Manual Printing Inventory by Online Printing Ø It reduces the Huge inventory in the Line Ø Spaces are saved with Discipline in Handling Ø Saved in Manpower with Optimum Utlisation in the Packing Lines 34
SUSTAINABILITY AND APPLICABILITY 35
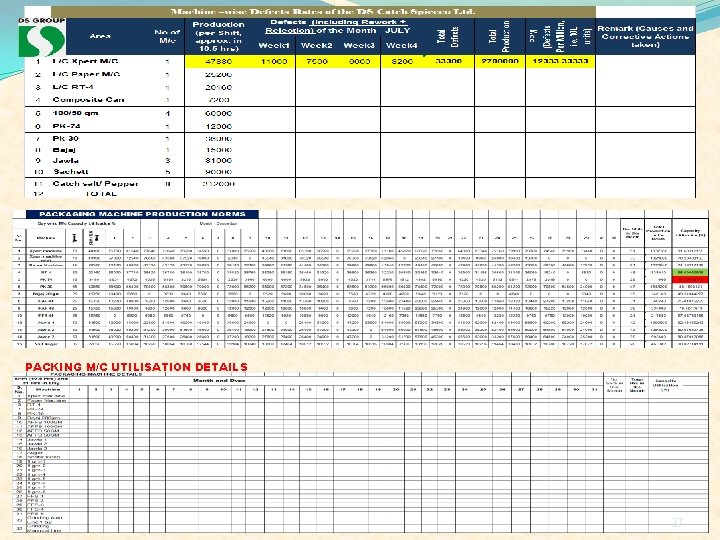
SUSTAINABILITY OVERALL EQUIPMENT EFFICIENCY CALCULATION DESIGN AND MAINTAIN OF MIS (Management Information System) Ø OEE Calculation of the Machines (Availability X Performance X Quality) Ø Control Chart with Corrective Action Ø Defects Calculation Chart 36
PACKING M/C UTILISATION DETAILS 37
The journey to 100 miles begins with a single step
39