2015 International Perforating Symposium Europe PENETRATION OF HIGH


- Slides: 30
2015 International Perforating Symposium Europe PENETRATION OF HIGH DENSITY TUNGSTEN BASE POROUS JETS MEIR MAYSELESS & DOV IPS-15 -7 1
2015 International Perforating Symposium Europe OUTLINE - INTRODUCTION - POWDERS - SIMULATIONS - CONCLUSIONS 2
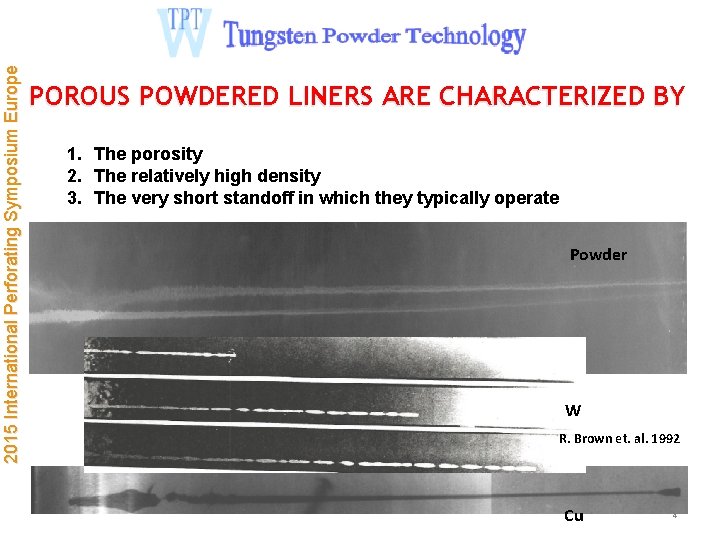
2015 International Perforating Symposium Europe POROUS POWDERED LINERS ARE BEING USED BECAUSE 1. The need to avoid plugging in the formed hole by the slug 2. The low cost of their production 3. The deep and wide penetration they achieve in the rock formation 4. The high efficiency of their penetration depth capabilities into rocks 3
2015 International Perforating Symposium Europe POROUS POWDERED LINERS ARE CHARACTERIZED BY 1. The porosity 2. The relatively high density 3. The very short standoff in which they typically operate Powder W R. Brown et. al. 1992 Cu 4
2015 International Perforating Symposium Europe POROUS POWDERED LINERS ARE CHARACTERIZED BY 1. 2. 3. 3. 4. 5. 6. Shape Density Porosity Composition of the liner material Size distribution and morphology of particles Type of powder (coated, strength, reactive…) Manufacturing process ALL THESE POINTS ARE CRUCIAL FOR ACHIEVING HIGH PERFORMANCES 5
2015 International Perforating Symposium Europe POROUS POWDERED JETS ARE CHARACTERIZED BY 1. 2. 3. 4. 5. The radial expansion The breakup phenomenon The density changes during flight The slug structure Their penetration characteristics 6
2015 International Perforating Symposium Europe RADIAL EXPANSION 750 m/s SCAN 1050 m/s 1230 m/s POROUS SCAN SOLID 7
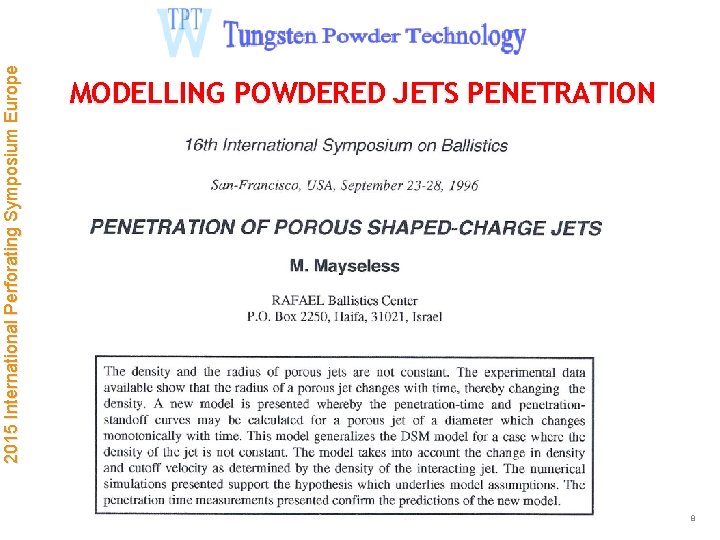
2015 International Perforating Symposium Europe MODELLING POWDERED JETS PENETRATION 8
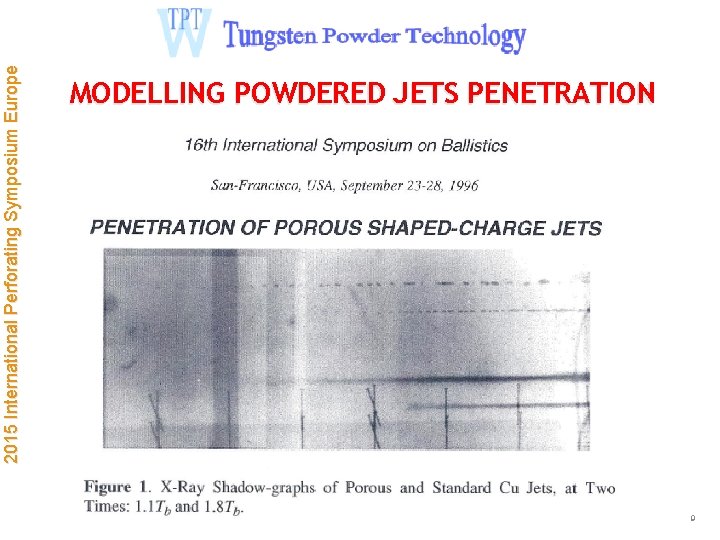
2015 International Perforating Symposium Europe MODELLING POWDERED JETS PENETRATION 9
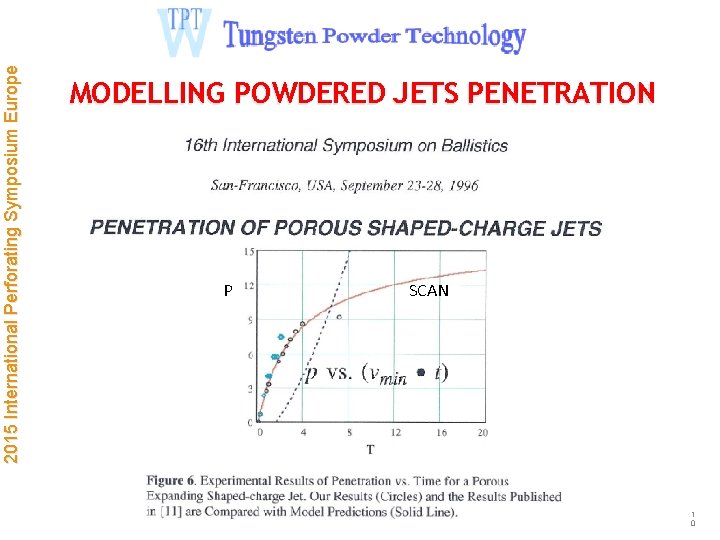
2015 International Perforating Symposium Europe MODELLING POWDERED JETS PENETRATION P SCAN 1 0
2015 International Perforating Symposium Europe WHY ARE POROUS POWDERED JETS SO EFFECTIVE? • MAIN REASONS: • High density jet tip to penetrate the Gun and the Case • At low density > low penetration rate > wider crater • No jet breakup > straight jet > enables longer jet and tail penetration 1 1
2015 International Perforating Symposium Europe OPERATIONAL METHODS CONSTAINS RESULTS IN: GENERALLY SPEAKING, AS A RESULT OF THE OPERATIONAL METHOD, THE JETS NEED TO BE LONG, HENCE THEIR TIP VELOCITY NEEDS TO BE HIGH. THE EFFECTIVE TAIL VELOCITY DEPENDS ON THE TARGET PROPERTIES, STRENGTH AND PRESSURE. TO ACHIEVE THESE REQUIREMENTS WE NEED TO OPERATE IN TWO MAIN DIRECTIONS: 1. DESIGN CORRECTLY THE SHAPED CHARGE GEOMETRY 2. USE THE CORRECT MATERIAL COMPOSITION THESE TWO REQUIREMENTS SHOULD BE COMBINED ! 12
2015 International Perforating Symposium Europe CHALLANGES The challenges today are greater than before since people started to recognize the importance of: 1. The internal pressure in the formation 2. The liquid or gas in the saturated rock 3. The exact morphology of the rock 4. The potential behind reactive jets 5. The very deep wells (temperature, pressure) 6. Crater channel profile 13
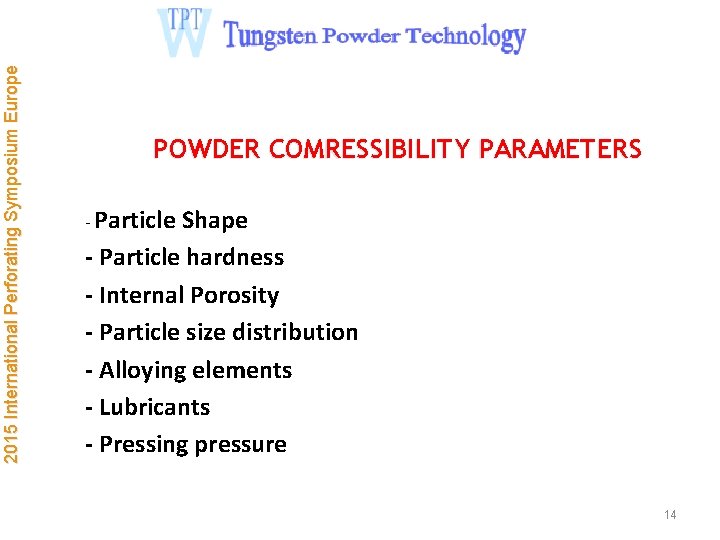
2015 International Perforating Symposium Europe POWDER COMRESSIBILITY PARAMETERS - Particle Shape - Particle hardness - Internal Porosity - Particle size distribution - Alloying elements - Lubricants - Pressing pressure 14
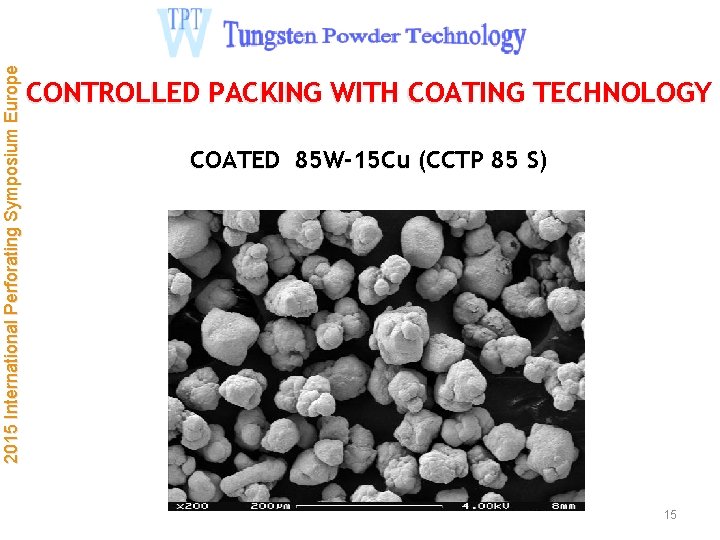
2015 International Perforating Symposium Europe CONTROLLED PACKING WITH COATING TECHNOLOGY COATED 85 W-15 Cu (CCTP 85 S) 15
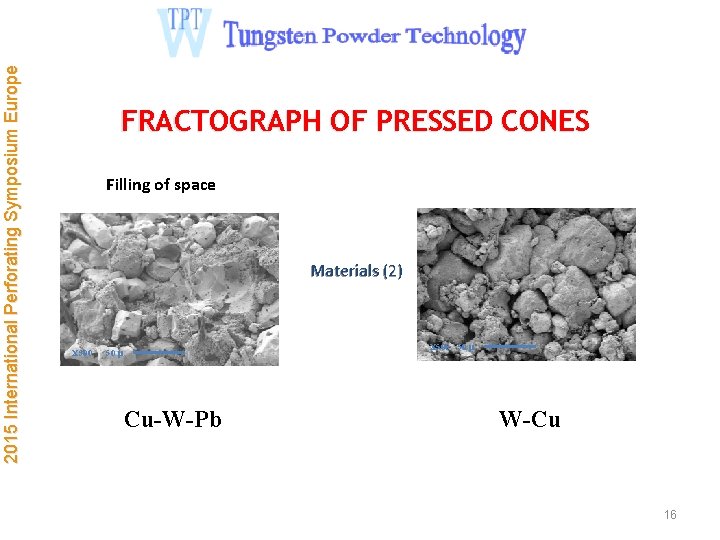
2015 International Perforating Symposium Europe FRACTOGRAPH OF PRESSED CONES Filling of space Materials (2) X 500 50 μ Cu-W-Pb W-Cu 16
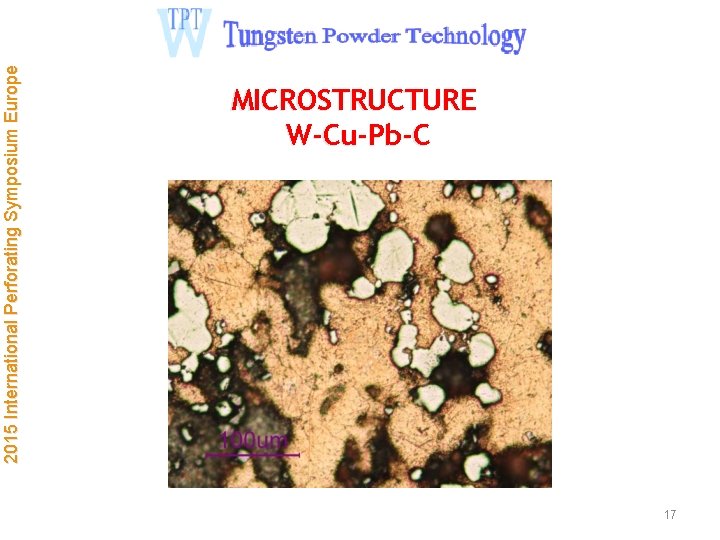
2015 International Perforating Symposium Europe MICROSTRUCTURE W-Cu-Pb-C 17
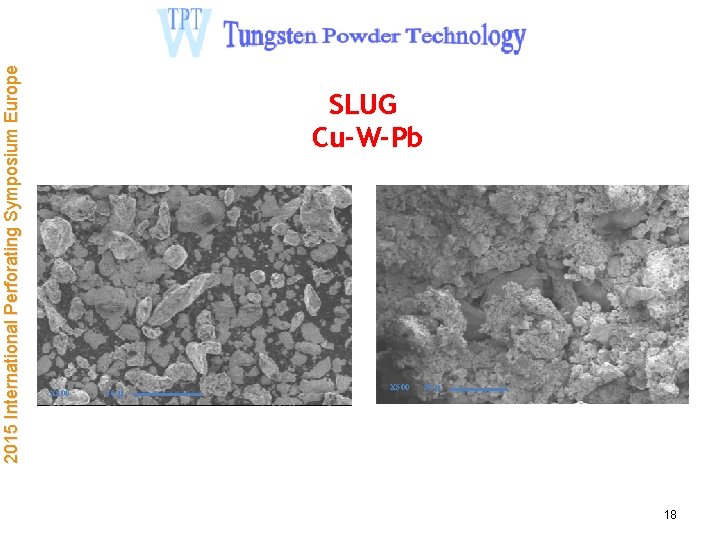
2015 International Perforating Symposium Europe SLUG Cu-W-Pb X 500 50 μ 18
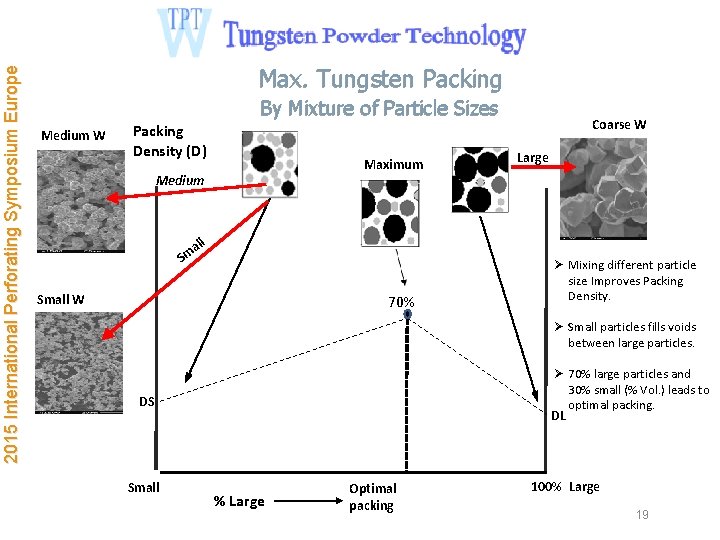
2015 International Perforating Symposium Europe Max. Tungsten Packing By Mixture of Particle Sizes Medium W Packing Density (D) Maximum Medium a Sm Coarse W Large ll Small W 70% Ø Mixing different particle size Improves Packing Density. Ø Small particles fills voids between large particles. Ø 70% large particles and 30% small (% Vol. ) leads to optimal packing. DL DS Small % Large Optimal packing 100% Large 19
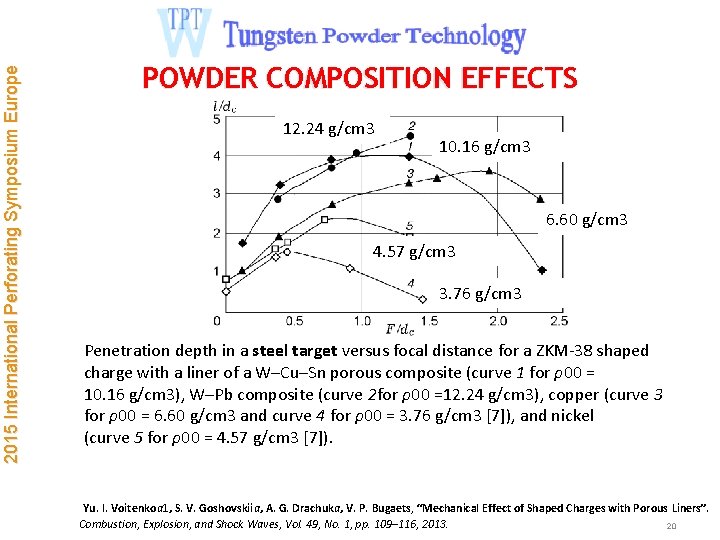
2015 International Perforating Symposium Europe POWDER COMPOSITION EFFECTS 12. 24 g/cm 3 10. 16 g/cm 3 6. 60 g/cm 3 4. 57 g/cm 3 3. 76 g/cm 3 Penetration depth in a steel target versus focal distance for a ZKM-38 shaped charge with a liner of a W–Cu–Sn porous composite (curve 1 for ρ00 = 10. 16 g/cm 3), W–Pb composite (curve 2 for ρ00 =12. 24 g/cm 3), copper (curve 3 for ρ00 = 6. 60 g/cm 3 and curve 4 for ρ00 = 3. 76 g/cm 3 [7]), and nickel (curve 5 for ρ00 = 4. 57 g/cm 3 [7]). Yu. I. Voitenkoa 1, S. V. Goshovskiia, A. G. Drachuka, V. P. Bugaets, “Mechanical Effect of Shaped Charges with Porous Liners”. Combustion, Explosion, and Shock Waves, Vol. 49, No. 1, pp. 109– 116, 2013. 20
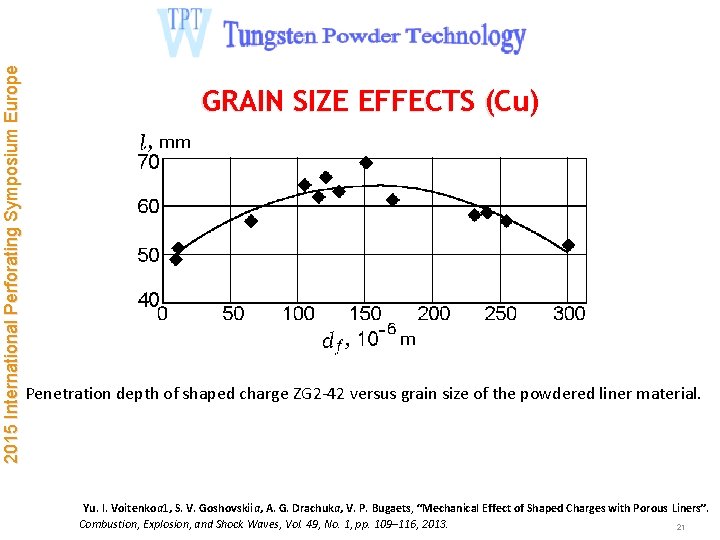
2015 International Perforating Symposium Europe GRAIN SIZE EFFECTS (Cu) Penetration depth of shaped charge ZG 2 -42 versus grain size of the powdered liner material. Yu. I. Voitenkoa 1, S. V. Goshovskiia, A. G. Drachuka, V. P. Bugaets, “Mechanical Effect of Shaped Charges with Porous Liners”. Combustion, Explosion, and Shock Waves, Vol. 49, No. 1, pp. 109– 116, 2013. 21
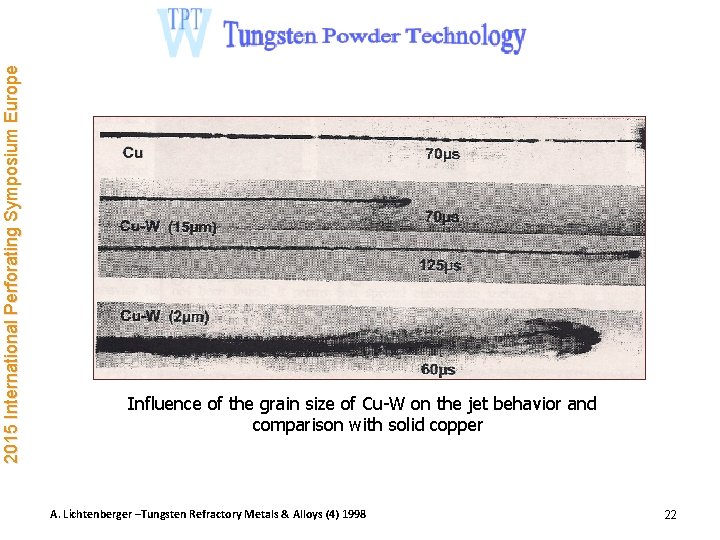
2015 International Perforating Symposium Europe Influence of the grain size of Cu-W on the jet behavior and comparison with solid copper A. Lichtenberger –Tungsten Refractory Metals & Alloys (4) 1998 22
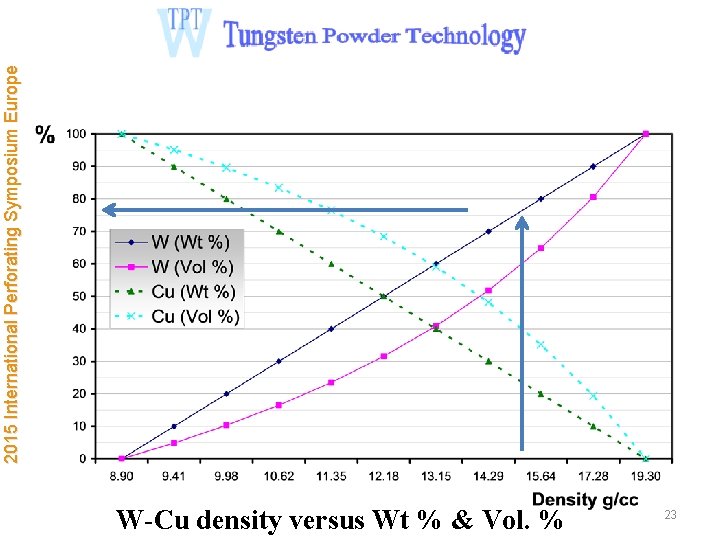
W-Cu density versus Wt % & Vol. % 23 2015 International Perforating Symposium Europe
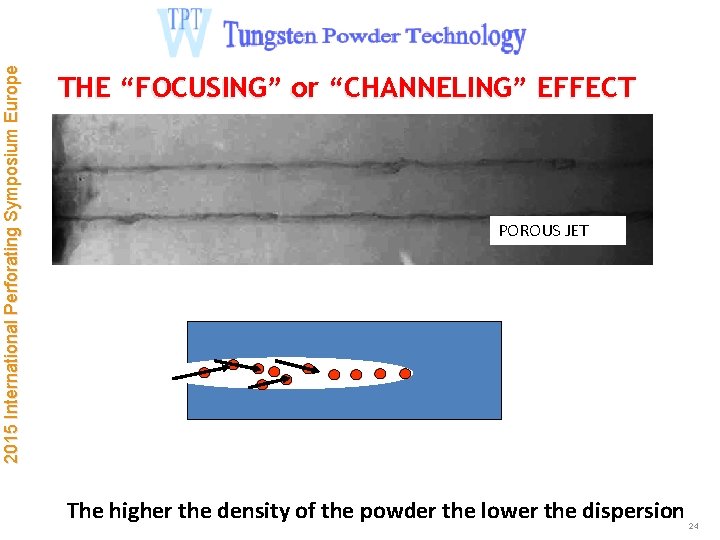
2015 International Perforating Symposium Europe THE “FOCUSING” or “CHANNELING” EFFECT POROUS JET The higher the density of the powder the lower the dispersion 24
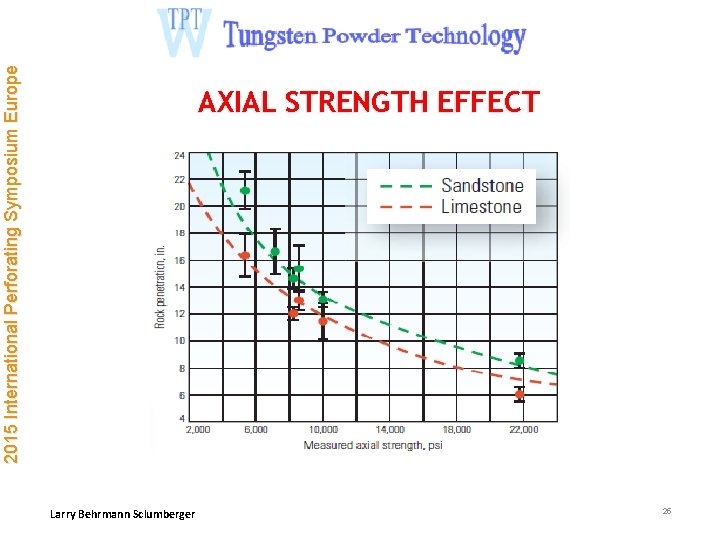
2015 International Perforating Symposium Europe AXIAL STRENGTH EFFECT Larry Behrmann Sclumberger 25
2015 International Perforating Symposium Europe ROCK PRESSURE AND STRENGTH EFFECTS • SMALLER CRATER • DELAYED AND LARGE COLLAPSE OF THE CRATER WALL THAT MIGHT DISTURBE THE SLOWER PARTS OF THE JET • HIGHER CUTOFF VELOCITY HOW TO COPE WITH THE PROBLEM? ? INNOVATION 26
2015 International Perforating Symposium Europe POROUS SC LINERS NEEDS New avenues: Hybrid liners Metal layer in the liner-explosive interface, for good mismatch Metal layer in the liner free interface to reduce jet radial expansion but to increase target radial enlargement. 27
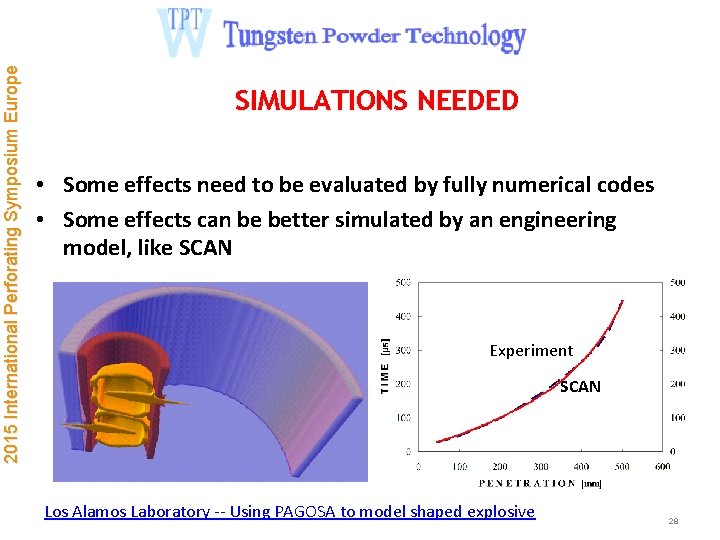
2015 International Perforating Symposium Europe SIMULATIONS NEEDED • Some effects need to be evaluated by fully numerical codes • Some effects can be better simulated by an engineering model, like SCAN Experiment SCAN Los Alamos Laboratory -- Using PAGOSA to model shaped explosive 28
2015 International Perforating Symposium Europe CONCLUSIONS High density porous jets were found to perform very well in soil materials. The penetration of a straight jet stops only if the jet cannot overcome the soil compression strength or if it becomes much wider than the crater width, causing a choking effect. In our opinion, porous jets can be further improved by employing a theoretical approach like the one applied here using the SCAN code and by employing the correct material blend for the liner 29
2015 International Perforating Symposium Europe THANKS 30