Thermally Conductive Foam and Foamcored Staves Tim Tested
- Slides: 15
Thermally Conductive Foam and Foam-cored Staves Tim
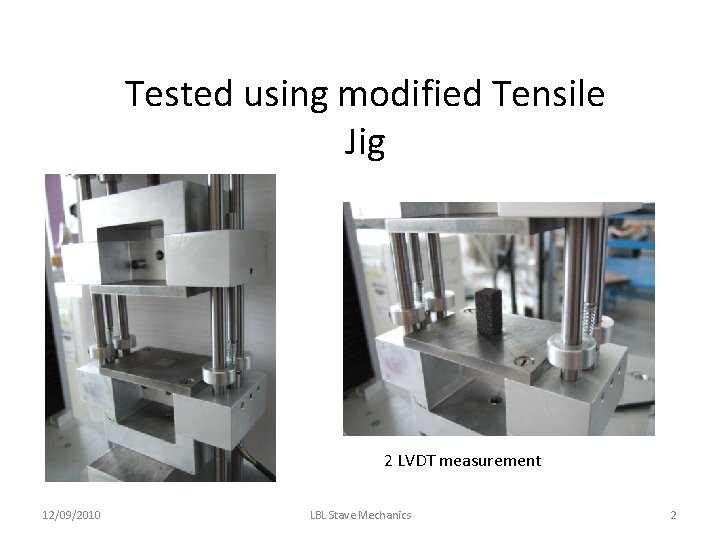
Tested using modified Tensile Jig 2 LVDT measurement 12/09/2010 LBL Stave Mechanics 2
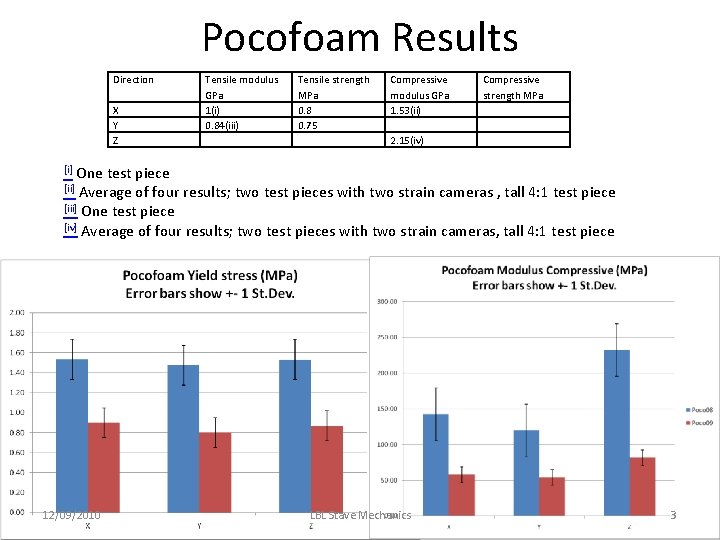
Pocofoam Results Direction X Y Z Tensile modulus GPa 1(i) 0. 84(iii) Tensile strength MPa 0. 8 0. 75 Compressive modulus GPa 1. 53(ii) Compressive strength MPa 2. 15(iv) One test piece [ii] Average of four results; two test pieces with two strain cameras , tall 4: 1 test piece [iii] One test piece [iv] Average of four results; two test pieces with two strain cameras, tall 4: 1 test piece [i] 12/09/2010 LBL Stave Mechanics 3
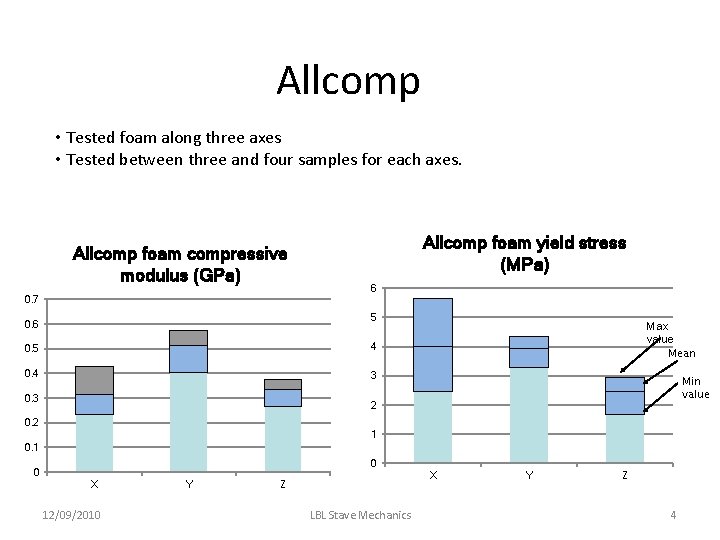
Allcomp • Tested foam along three axes • Tested between three and four samples for each axes. Allcomp foam compressive modulus (GPa) 0. 7 Allcomp foam yield stress (MPa) 6 5 0. 6 0. 5 4 0. 4 3 0. 3 Max value Mean Min value 2 0. 2 1 0 0 X 12/09/2010 Y X Z LBL Stave Mechanics Y Z 4
Foam Cores – Plank 4 • Plank#4 has – Co-cured tapes – Graftech Grafoam FPA-02 carbon foam (0. 03 g/cm 3) instead of honeycomb • Glued in foam core last Friday • Glued in after Pocofoam/pipes/close-outs, using unloaded Hysol – Foam machined to sections ~300 mm long, ~twice nominal height. – Use scraper with narrow 150μm stand-offs – Used 28. 7 g glue (this is ~twice as much as for honeycomb) • Mill to height today, then glue on top skin (don’t know how to apply two different kinds of glues, might just go for BN-loaded glue everywhere). • Planning to make plank#5 with corrugated core. 5
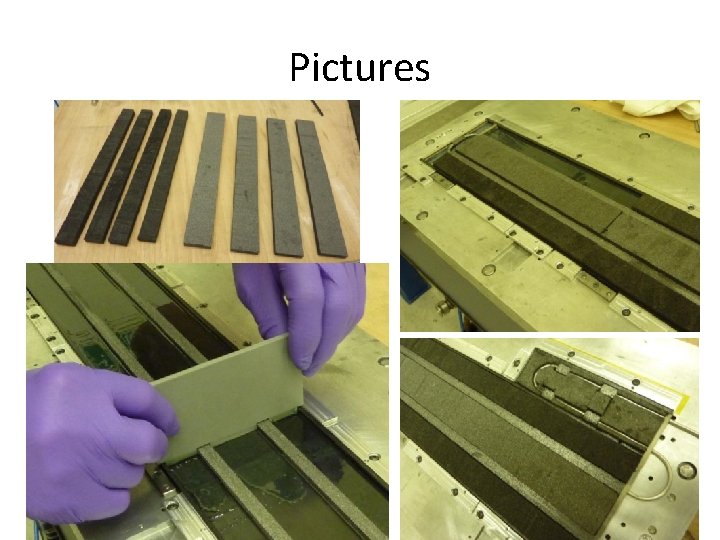
Pictures 6
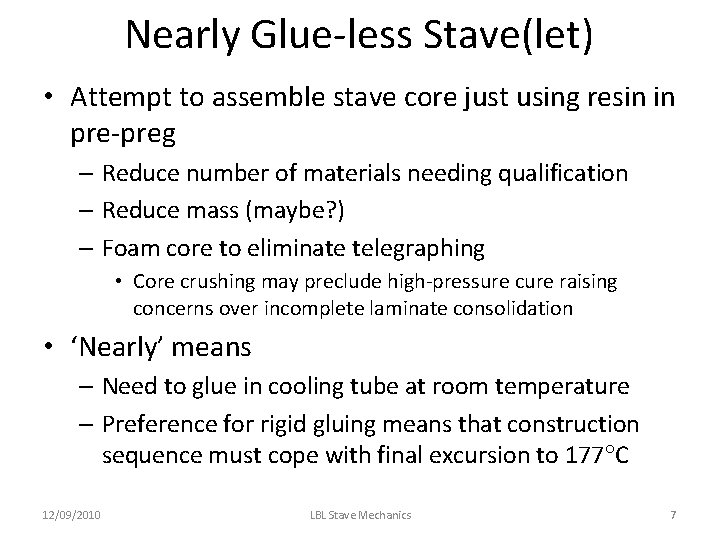
Nearly Glue-less Stave(let) • Attempt to assemble stave core just using resin in pre-preg – Reduce number of materials needing qualification – Reduce mass (maybe? ) – Foam core to eliminate telegraphing • Core crushing may preclude high-pressure cure raising concerns over incomplete laminate consolidation • ‘Nearly’ means – Need to glue in cooling tube at room temperature – Preference for rigid gluing means that construction sequence must cope with final excursion to 177 C 12/09/2010 LBL Stave Mechanics 7
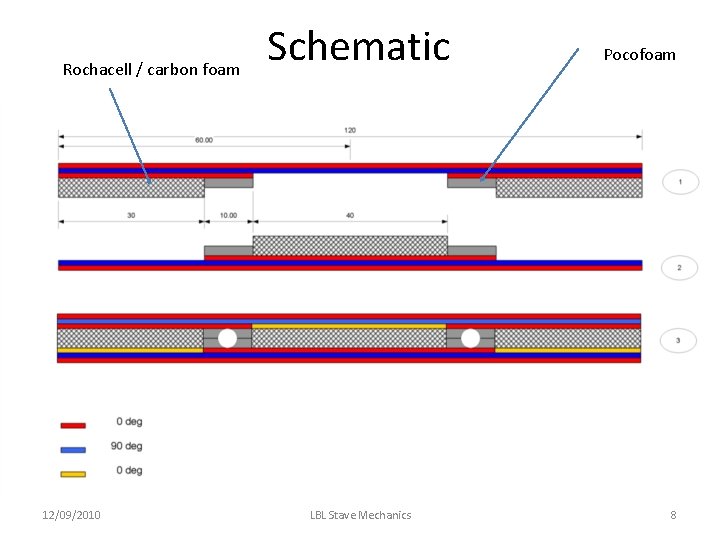
Rochacell / carbon foam 12/09/2010 Schematic LBL Stave Mechanics Pocofoam 8
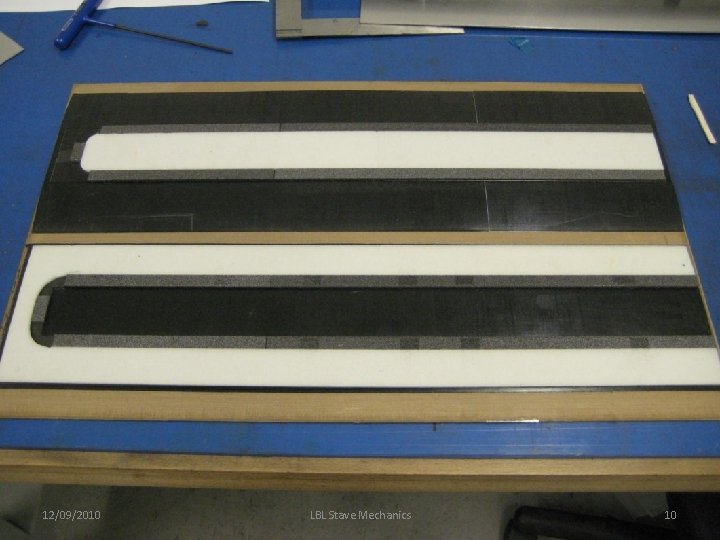
Construction Steps 1. Prepare first side – – Lay up 0/90 over full width Lay up 0 in two 40 mm wide strips down both sides Add 10 mm wide Pocofoam and 30 mm wide Rohacell Cure at 177 C under vacuum for 2 hours 2. Prepare second side – – 12/09/2010 Lay up 0/90 over full width Lay up 0 in one central strip of width 60 mm Add 10 mm wide Pocofoam and 40 mm wide Rohacell Cure at 177 C under vacuum for 2 hours LBL Stave Mechanics 9
12/09/2010 LBL Stave Mechanics 10
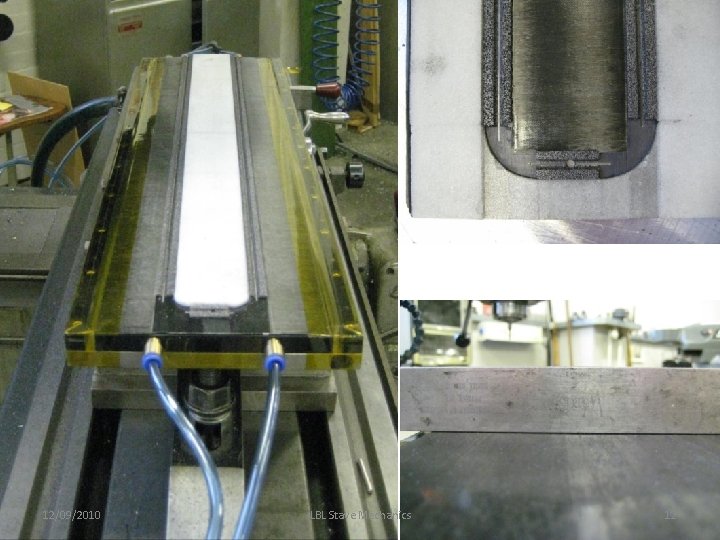
Next Steps 3. Add cooling channels – Trim to just > 120 mm wide – Dowel up both sides to vacuum jig – Grind Rohacell down to 3. 2 mm – Grind/mill Pocofoam down to 1. 6 mm – Form R 1. 6 channel in Pocofoam • Possible further refinement may be to mill channel at R 1. 66 and co cure in layer of 0 deg fibres. – This could allow CGL to be used without worrying about loss into Pocofoam? 12/09/2010 LBL Stave Mechanics 11
12/09/2010 LBL Stave Mechanics 12
Final Co-cure 4. Final co-cure (step 3 in cartoon) – Add glue and tube into channel (Titanium) – Add final 0 -degree layers to complete 3 -ply face sheets – Vacuum bag – Leave for 24 -48 h for glue to cure – Final co-cure at 177 C for 2 hours under vacuum – Expect to complete next week 12/09/2010 LBL Stave Mechanics 13
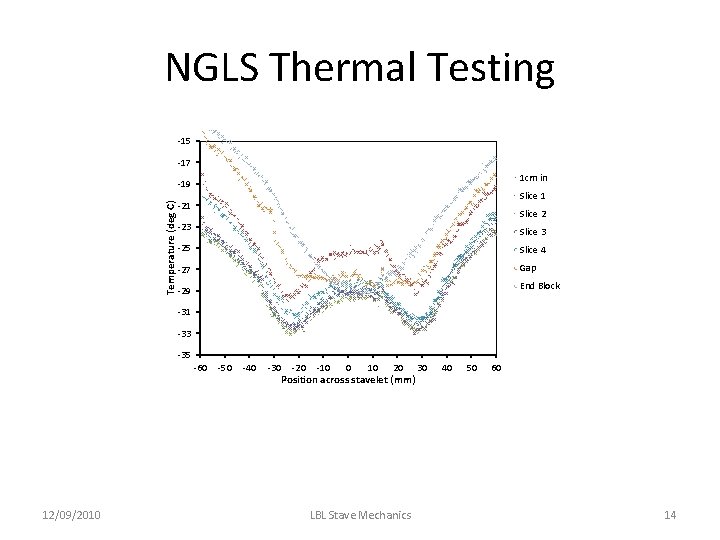
NGLS Thermal Testing -15 -17 1 cm in Temperature (deg C) -19 Slice 1 -21 Slice 2 -23 Slice 3 -25 Slice 4 -27 Gap -29 End Block -31 -33 -35 -60 12/09/2010 -50 -40 -30 -20 -10 0 10 20 Position across stavelet (mm) LBL Stave Mechanics 30 40 50 60 14
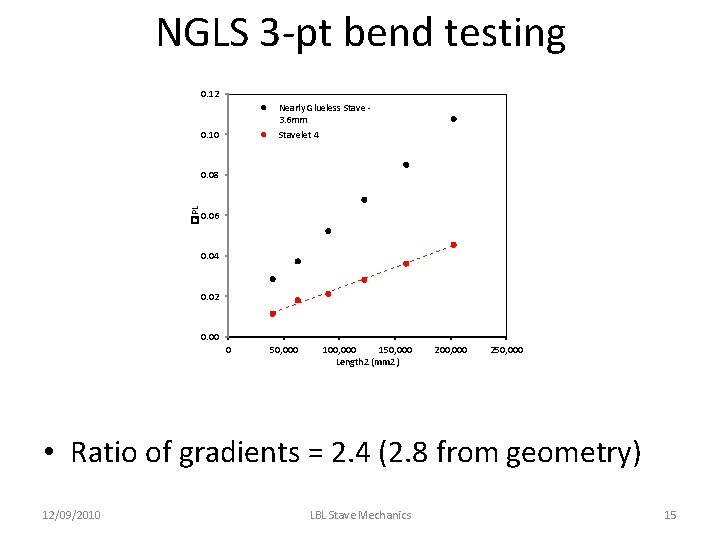
NGLS 3 -pt bend testing 0. 12 Nearly Glueless Stave 3. 6 mm Stavelet 4 0. 10 �/PL 0. 08 0. 06 0. 04 0. 02 0. 00 0 50, 000 100, 000 150, 000 Length 2 (mm 2) 200, 000 250, 000 • Ratio of gradients = 2. 4 (2. 8 from geometry) 12/09/2010 LBL Stave Mechanics 15