API 16 AR Specification for Drillthrough Equipment Remanufacturing
- Slides: 5
API 16 AR Specification for Drillthrough Equipment Remanufacturing Summer Standards Meeting Communication Jan van Wijk / Chris Johnson API-16 AR chairman Janvanwijk@Shell. com / Chris. Johnson@nov. com 25 June , 2013 1
Status 1. Draft document 50% state. 2. Task groups formed to work compile standard content on Welding, flow diagrams and certification. 3. Meetings planned for welding subgroup and next face to face end August. 4. Establishment of Material Data Book and Project History File as part of the API-16 AR standard is essential for traceability. Completion time governed by welding subgroup progress on the subject. 5. Complete draft document to be worked on in the August face to face meeting. 6. Acceptance for Quality Specification Levels for remanufacturing process. 7. Strong drive to deliver the standard for Ballot end 2013. 1220 L Street, NW • Washington, DC 20005 -4070 • www. api. org 2
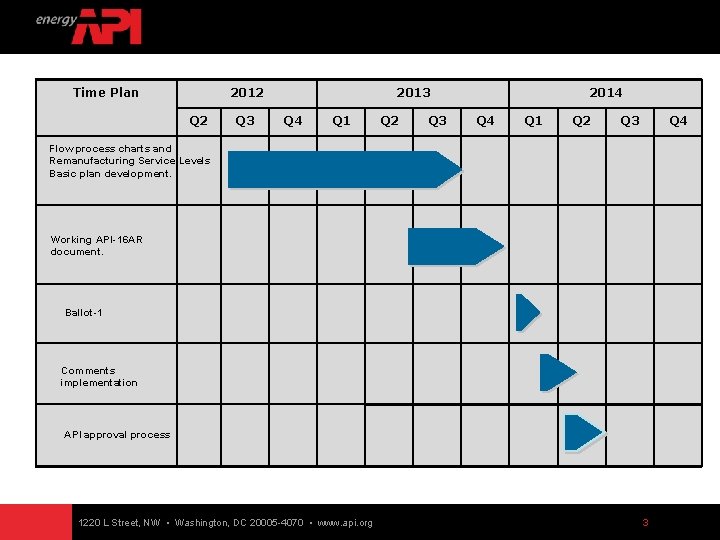
Time Plan 2012 Q 3 2013 Q 4 Q 1 Q 2 Q 3 2014 Q 1 Q 2 Q 3 Q 4 Flow process charts and Remanufacturing Service Levels Basic plan development. Working API-16 AR document. Ballot-1 Comments implementation API approval process 1220 L Street, NW • Washington, DC 20005 -4070 • www. api. org 3
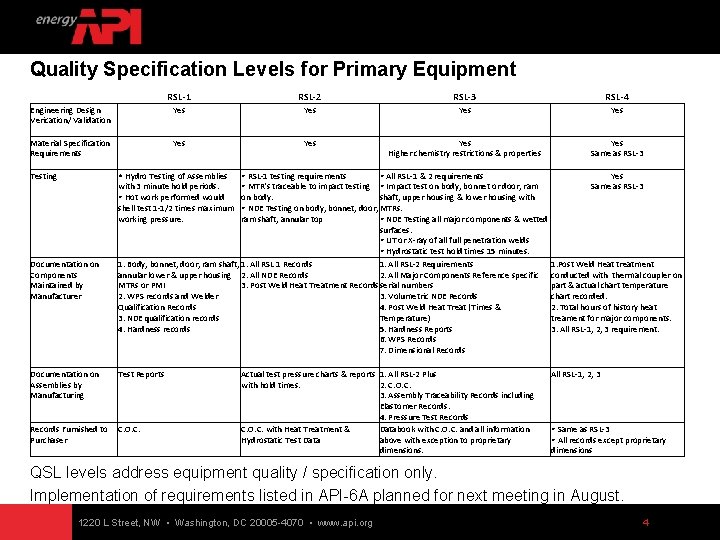
Quality Specification Levels for Primary Equipment RSL-1 RSL-2 RSL-3 RSL-4 Engineering Design Verication/ Validation Yes Yes Material Specification Requirements Yes Yes Higher chemistry restrictions & properties Yes Same as RSL-3 • Hydro Testing of Assemblies Testing • RSL-1 testing requirements • All RSL-1 & 2 requirements • MTR's traceable to impact testing • Impact test on body, bonnet or door, ram on body. shaft, upper housing & lower housing with • NDE Testing on body, bonnet, door, MTRs. ram shaft, annular top • NDE Testing all major components & wetted surfaces. • UT or X-ray of all full penetration welds • Hydrostatic test hold times 15 minutes. 1. Body, bonnet, door, ram shaft, 1. All RSL 1 Records 1. All RSL-2 Requirements annular lower & upper housing 2. All NDE Records 2. All Major Components Reference specific MTRs or PMI 3. Post Weld Heat Treatment Records serial numbers 2. WPS records and Welder 3. Volumetric NDE Records Qualification Records 4. Post Weld Heat Treat (Times & 3. NDE qualification records Temperature) 4. Hardness records 5. Hardness Reports 6. WPS Records 7. Dimensional Records with 3 minute hold periods. • Hot work performed would shell test 1 -1/2 times maximum working pressure. Documentation on Components Maintained by Manufacturer Documentation on Assemblies by Manufacturing Test Reports Records Furnished to Purchaser C. O. C. Actual test pressure charts & reports 1. All RSL-2 Plus with hold times. 2. C. O. C. 3. Assembly Traceability Records including Elastomer Records. 4. Pressure Test Records C. O. C. with Heat Treatment & Databook with C. O. C. and all information Hydrostatic Test Data above with exception to proprietary dimensions. Yes Same as RSL-3 1. Post Weld Heat treatment conducted with thermal coupler on part & actual chart temperature chart recorded. 2. Total hours of history heat treament for major components. 3. All RSL-1, 2, 3 requirement. All RSL-1, 2, 3 • Same as RSL-3 • All records except proprietary dimensions QSL levels address equipment quality / specification only. Implementation of requirements listed in API-6 A planned for next meeting in August. 1220 L Street, NW • Washington, DC 20005 -4070 • www. api. org 4
Q&A… • For information, please contact API directly or contact: Jan van Wijk API-16 AR chairman Janvanwiijk@shell. com Chris Johnson API-16 AR co-chairman Chris. johnson@nov. com 1220 L Street, NW • Washington, DC 20005 -4070 • www. api. org 5