
MINOS Detector Scintillator Module Construction Methods Jim Grudzinski
- Slides: 35
MINOS Detector Scintillator Module Construction Methods Jim Grudzinski Mechanical Engineer Argonne National Laboratory High Energy Physics division (for the MINOS Collaboration) 1
Some Motivation p The MINOS detector has a very large solid scintillator area-28, 000 m 2 (0. 3 k. T) n n 8 x times larger than anything previous (Grand Sasso -3600 m 2) This size could only be accomplished with improved strategies Extruded Scinitillator p High Quality WLS fiber p low cost multi-pixel PMT’s p Efficient and low-cost production techniques p 2
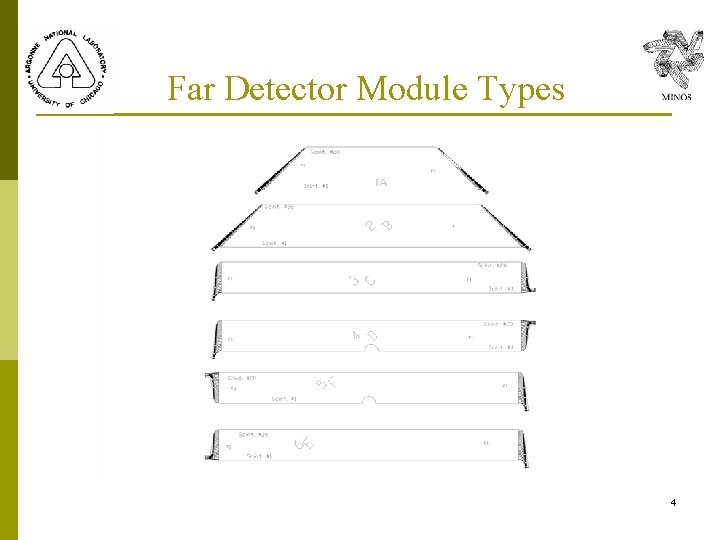
Some Design Considerations § 4445 Modules required § § § 3782 Far Detector, 4 types plus two mirror images, 20 - to 28 strips wide, 8 m long 573 Near Detector, 8 types plus 8 mirror images, 16 -, 20 -, and 28 - strips wide, 2 -3. 6 m long Flexible assembly methods required to accomodate variety in size and geometry Quality and consistency needed for large scale production Cost kept down through lower cost student labor § Unskilled (initially) labor 3
Far Detector Module Types 4
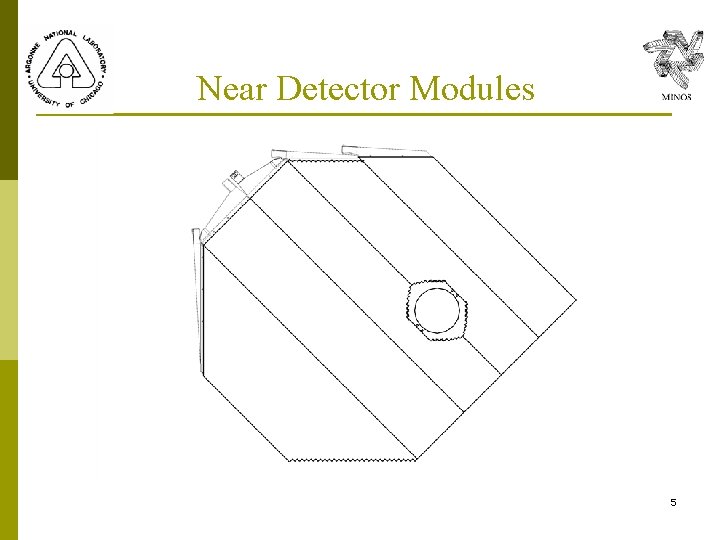
Near Detector Modules 5
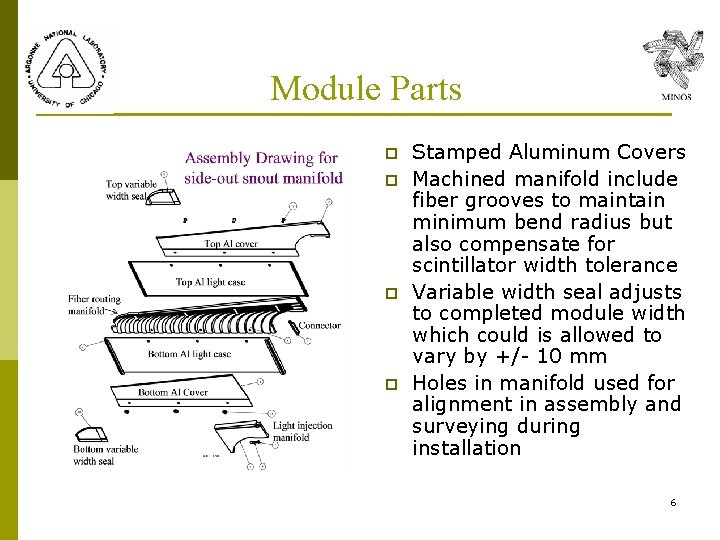
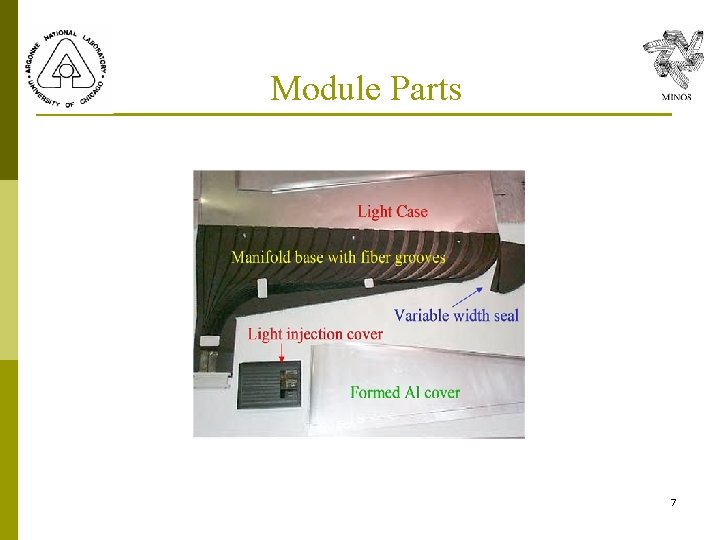
Module Parts p p Stamped Aluminum Covers Machined manifold include fiber grooves to maintain minimum bend radius but also compensate for scintillator width tolerance Variable width seal adjusts to completed module width which could is allowed to vary by +/- 10 mm Holes in manifold used for alignment in assembly and surveying during installation 6
Module Parts 7
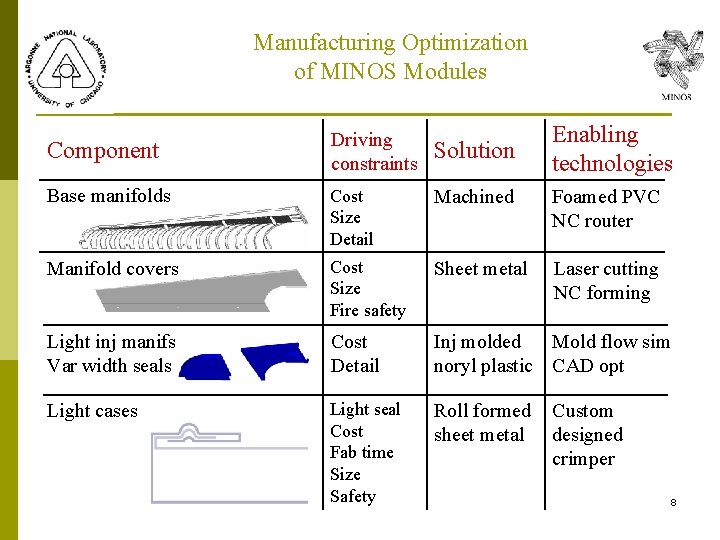
Manufacturing Optimization of MINOS Modules Enabling technologies Component Driving constraints Solution Base manifolds Cost Size Detail Machined Foamed PVC NC router Manifold covers Cost Size Fire safety Sheet metal Laser cutting NC forming Light inj manifs Var width seals Cost Detail Inj molded Mold flow sim noryl plastic CAD opt Light cases Light seal Cost Fab time Size Safety Roll formed sheet metal Custom designed crimper 8
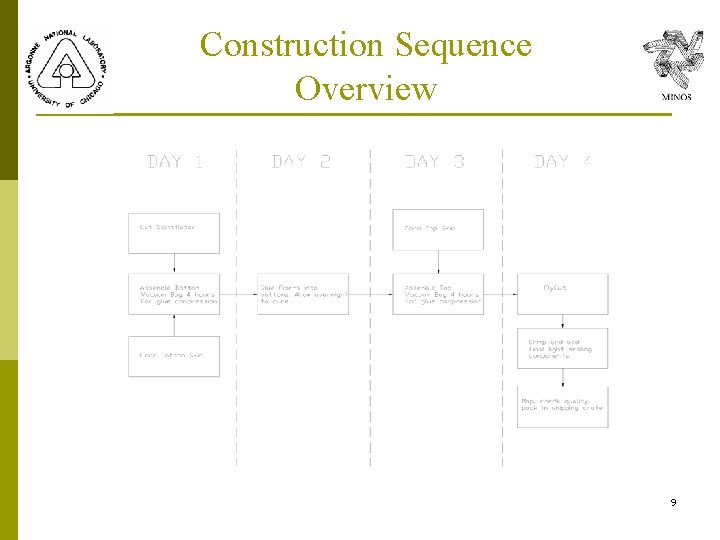
Construction Sequence Overview 9
MINOS Module Assembly Equipment p p p p Scintillator cutting station Forming Station Assembly trays Module curing racks Fiber gluing machine Connector flycutter Module Crimper Module Source Mapper 10
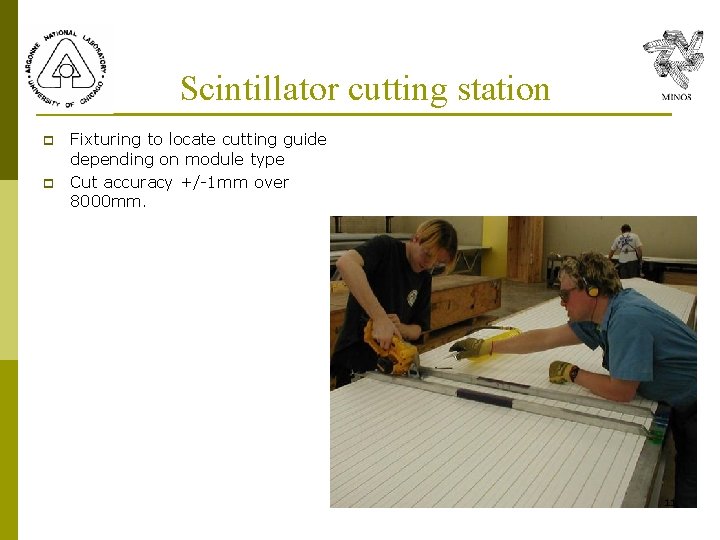
Scintillator cutting station p p Fixturing to locate cutting guide depending on module type Cut accuracy +/-1 mm over 8000 mm. 11
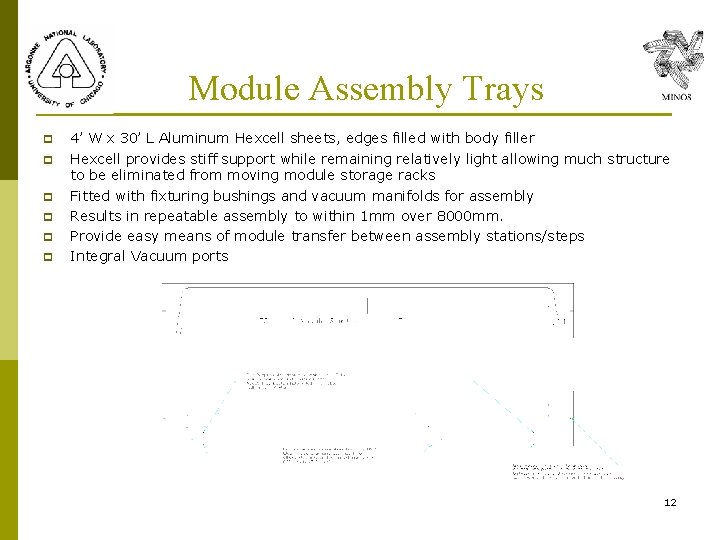
Module Assembly Trays p p p 4’ W x 30’ L Aluminum Hexcell sheets, edges filled with body filler Hexcell provides stiff support while remaining relatively light allowing much structure to be eliminated from moving module storage racks Fitted with fixturing bushings and vacuum manifolds for assembly Results in repeatable assembly to within 1 mm over 8000 mm. Provide easy means of module transfer between assembly stations/steps Integral Vacuum ports 12
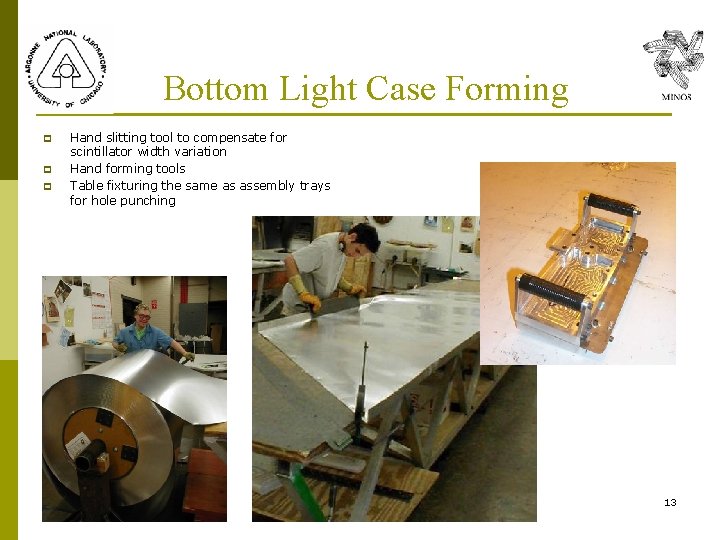
Bottom Light Case Forming p p p Hand slitting tool to compensate for scintillator width variation Hand forming tools Table fixturing the same as assembly trays for hole punching 13
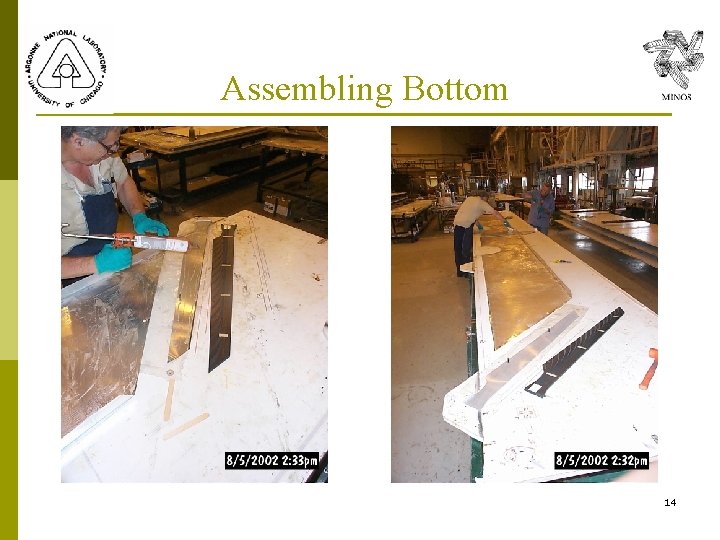
Assembling Bottom 14
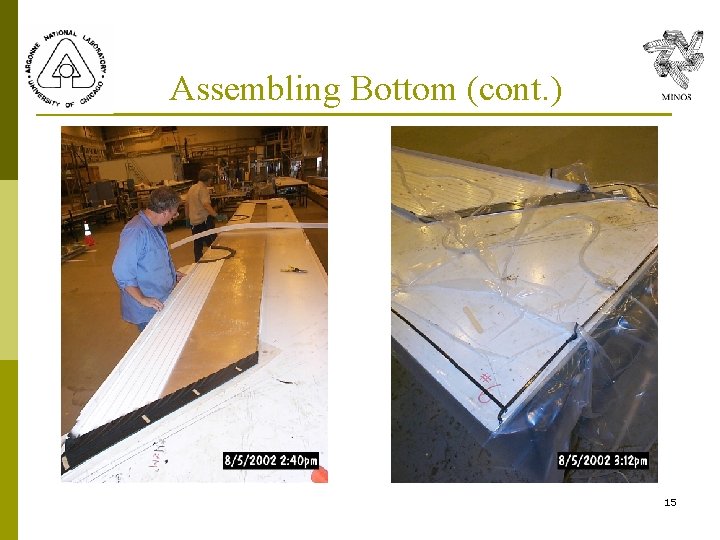
Assembling Bottom (cont. ) 15
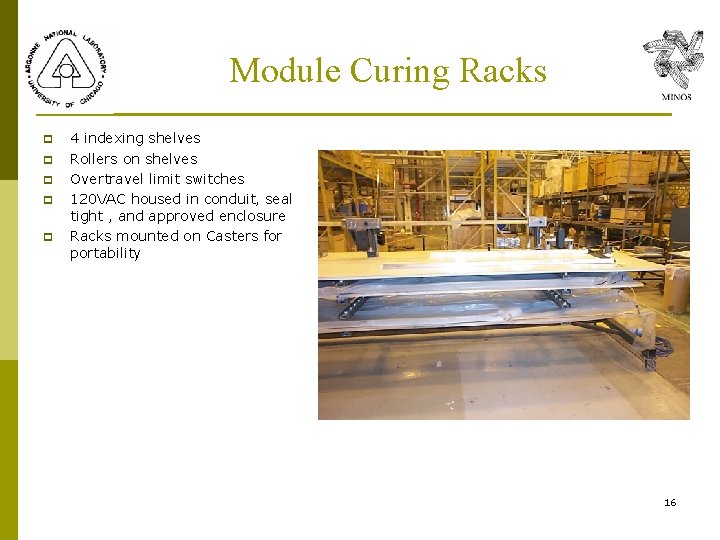
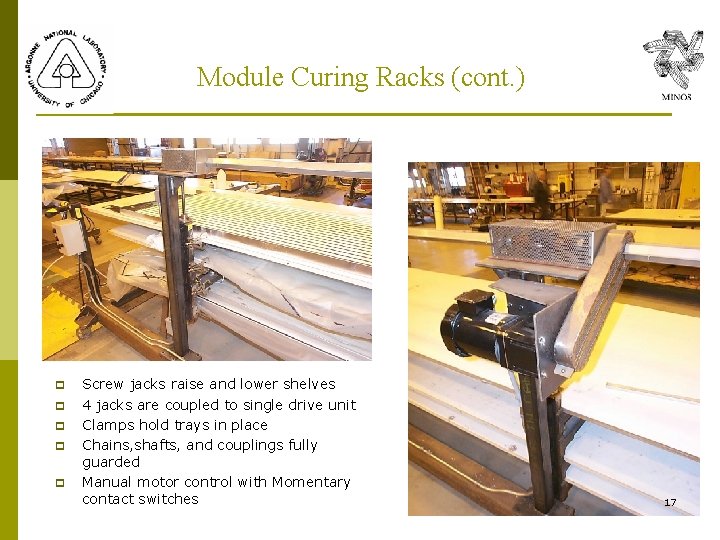
Module Curing Racks p p p 4 indexing shelves Rollers on shelves Overtravel limit switches 120 VAC housed in conduit, seal tight , and approved enclosure Racks mounted on Casters for portability 16
Module Curing Racks (cont. ) p p p Screw jacks raise and lower shelves 4 jacks are coupled to single drive unit Clamps hold trays in place Chains, shafts, and couplings fully guarded Manual motor control with Momentary contact switches 17
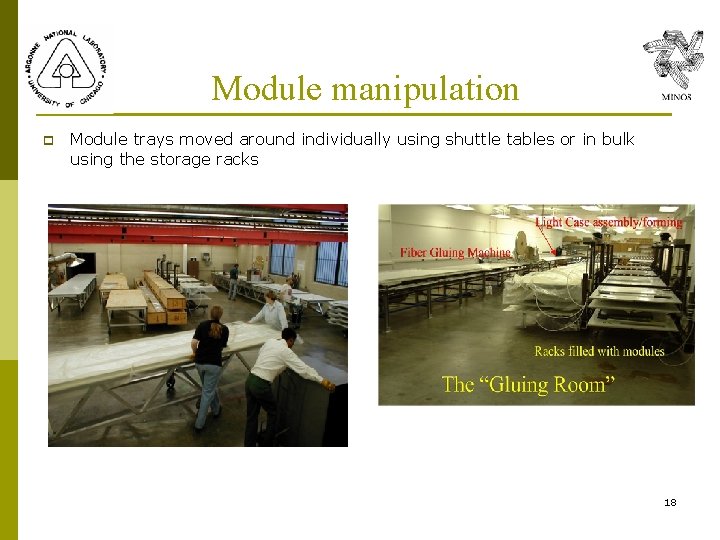
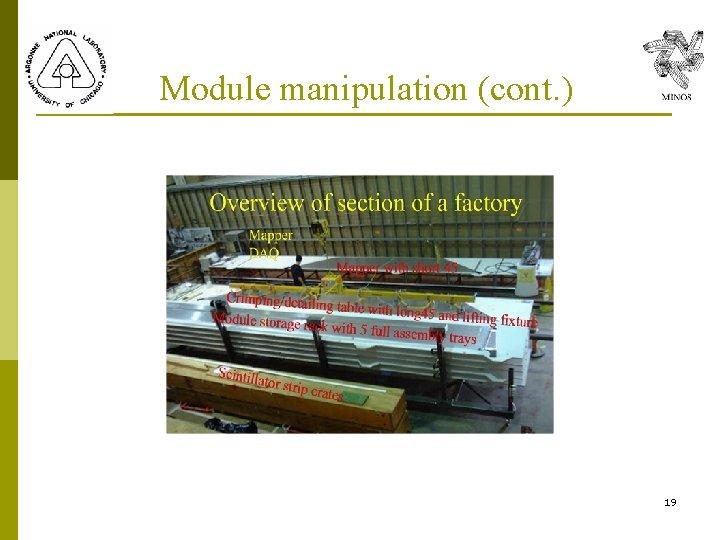
Module manipulation p Module trays moved around individually using shuttle tables or in bulk using the storage racks 18
Module manipulation (cont. ) 19
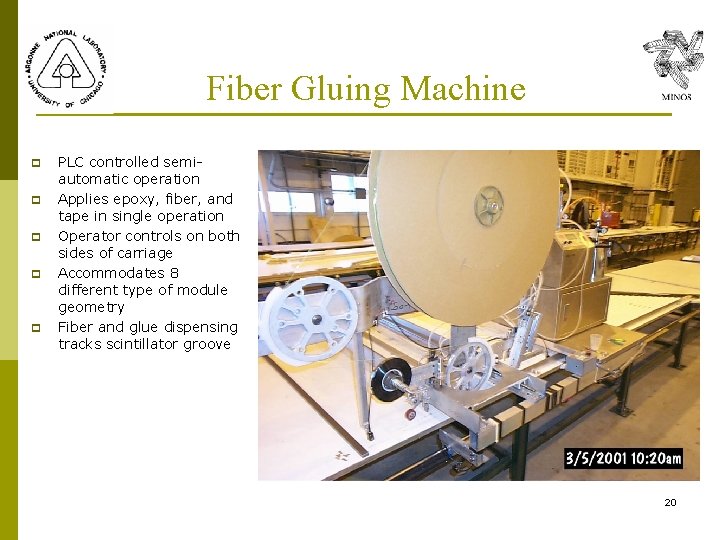
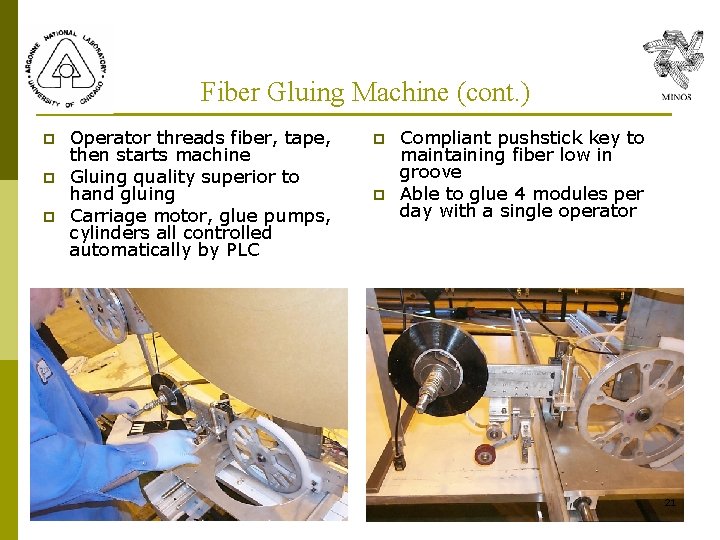
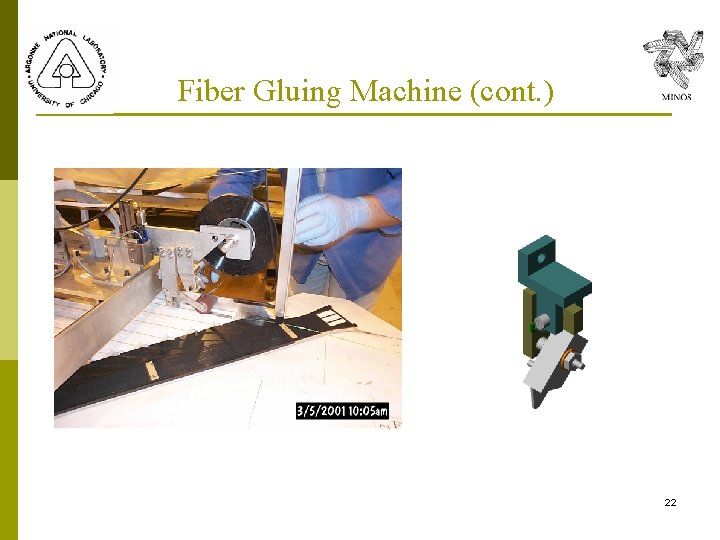
Fiber Gluing Machine p p p PLC controlled semiautomatic operation Applies epoxy, fiber, and tape in single operation Operator controls on both sides of carriage Accommodates 8 different type of module geometry Fiber and glue dispensing tracks scintillator groove 20
Fiber Gluing Machine (cont. ) p p p Operator threads fiber, tape, then starts machine Gluing quality superior to hand gluing Carriage motor, glue pumps, cylinders all controlled automatically by PLC p p Compliant pushstick key to maintaining fiber low in groove Able to glue 4 modules per day with a single operator 21
Fiber Gluing Machine (cont. ) 22
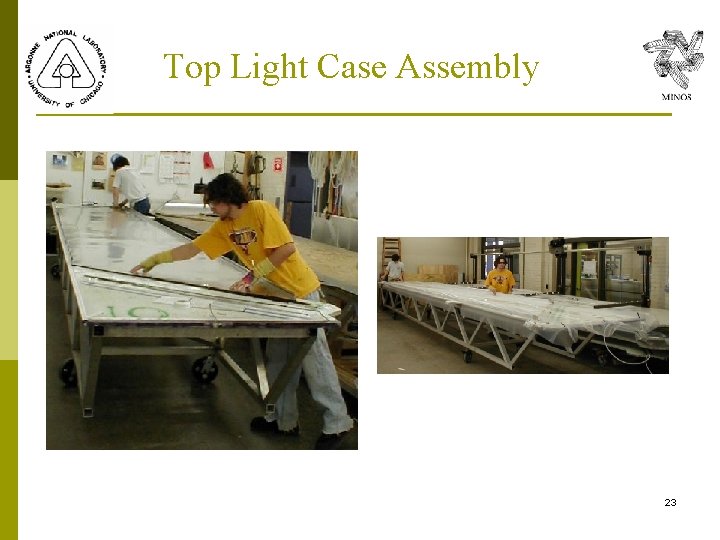
Top Light Case Assembly 23
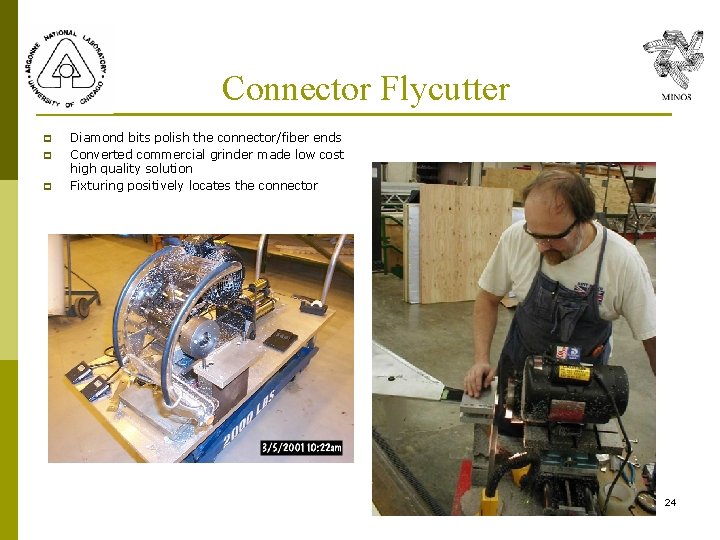
Connector Flycutter p p p Diamond bits polish the connector/fiber ends Converted commercial grinder made low cost high quality solution Fixturing positively locates the connector 24
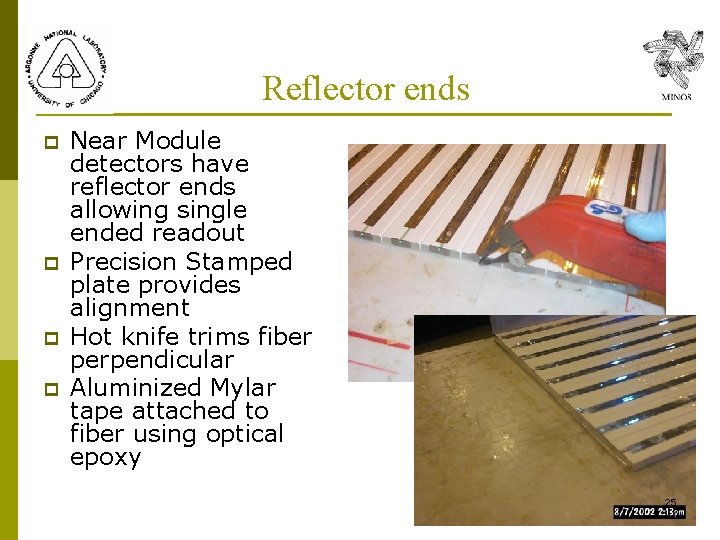
Reflector ends p p Near Module detectors have reflector ends allowing single ended readout Precision Stamped plate provides alignment Hot knife trims fiber perpendicular Aluminized Mylar tape attached to fiber using optical epoxy 25
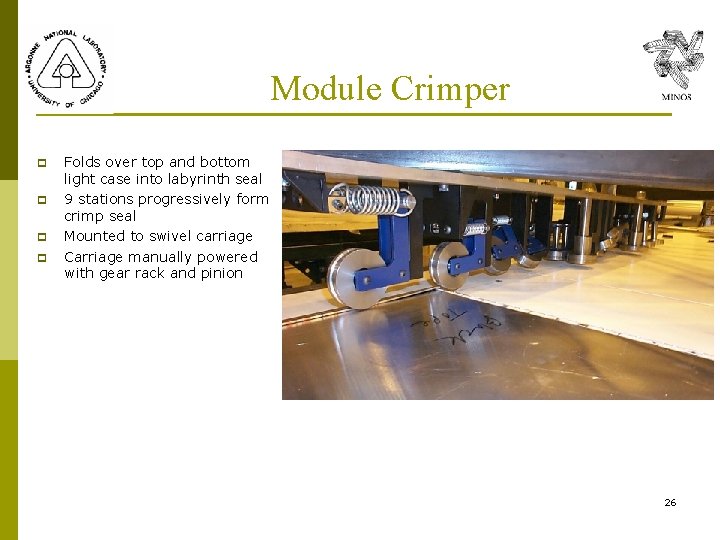
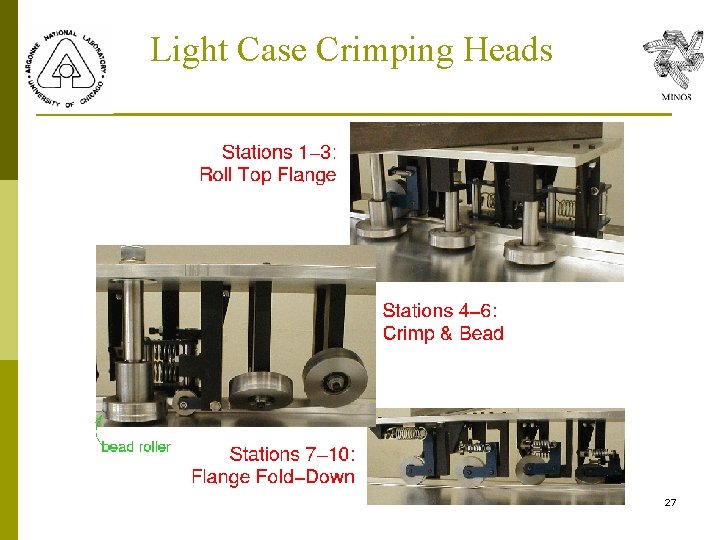
Module Crimper p p Folds over top and bottom light case into labyrinth seal 9 stations progressively form crimp seal Mounted to swivel carriage Carriage manually powered with gear rack and pinion 26
Light Case Crimping Heads 27
Light Case Crimp: Cutaway View 28
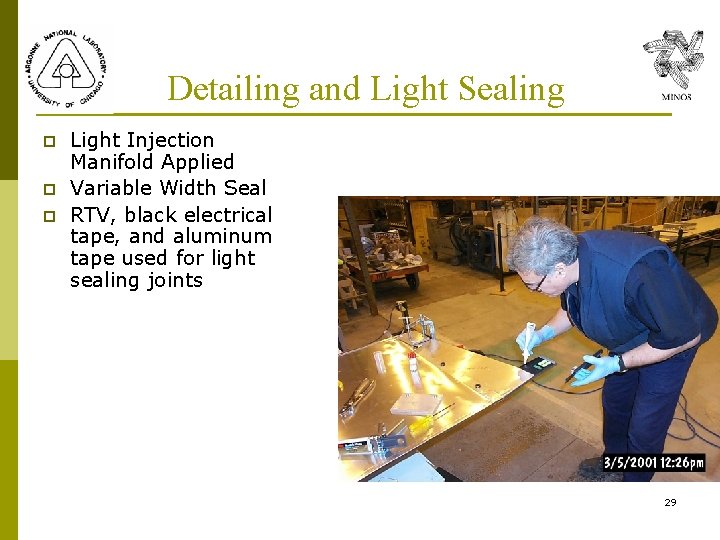
Detailing and Light Sealing p p p Light Injection Manifold Applied Variable Width Seal RTV, black electrical tape, and aluminum tape used for light sealing joints 29
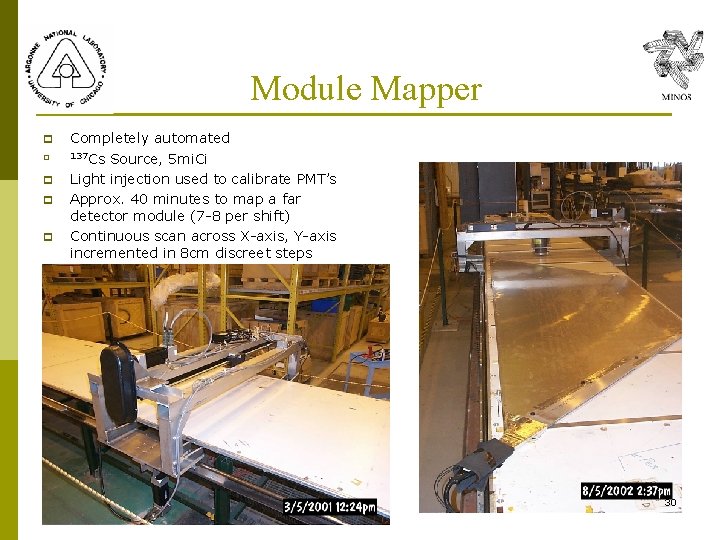
Module Mapper p p p Completely automated 137 Cs Source, 5 mi. Ci Light injection used to calibrate PMT’s Approx. 40 minutes to map a far detector module (7 -8 per shift) Continuous scan across X-axis, Y-axis incremented in 8 cm discreet steps 30
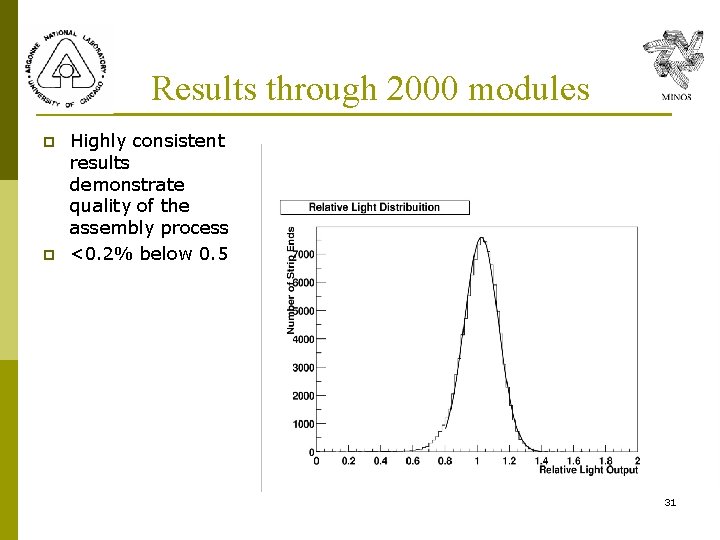
Results through 2000 modules p p Highly consistent results demonstrate quality of the assembly process <0. 2% below 0. 5 31
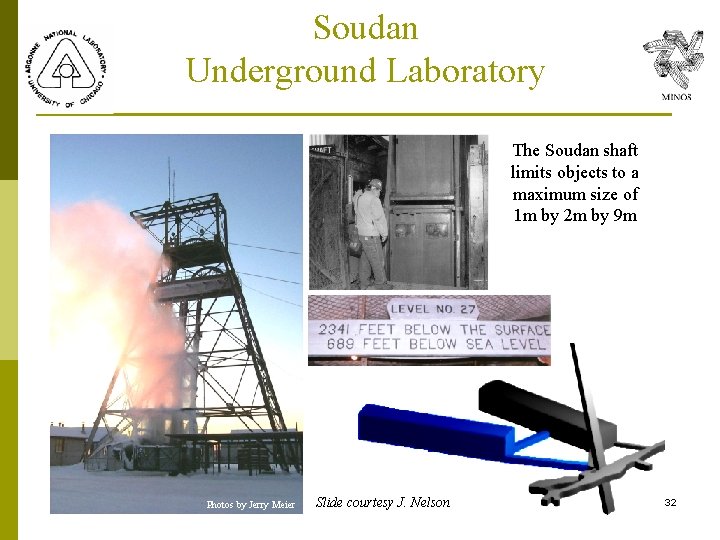
Soudan Underground Laboratory The Soudan shaft limits objects to a maximum size of 1 m by 2 m by 9 m Photos by Jerry Meier Slide courtesy J. Nelson 32
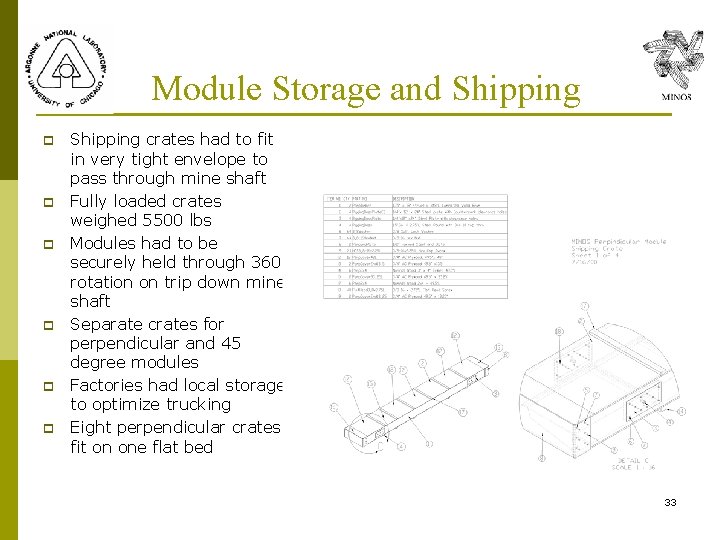
Module Storage and Shipping p p p Shipping crates had to fit in very tight envelope to pass through mine shaft Fully loaded crates weighed 5500 lbs Modules had to be securely held through 360 rotation on trip down mine shaft Separate crates for perpendicular and 45 degree modules Factories had local storage to optimize trucking Eight perpendicular crates fit on one flat bed 33
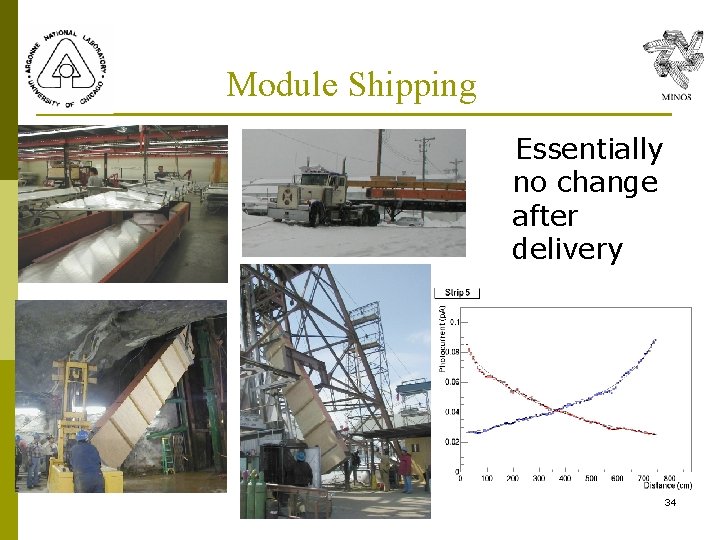
Module Shipping Essentially no change after delivery 34
Conclusion p High precision large scale assembly was accomplished using lower cost unskilled labor through creative use of tooling n n n p Assembly trays allowed tight envelope tolerance Crimping provided reliable and fast light tight seal Hand forming allowed custom module widths Automatic mapping required minimal manpower Laminated assembly technique made stiff modules Automated Fiber gluing combined with extruded scintuillator produced high quality consistent modules Resulting Modules show high quality and consistency with 75% of the production complete 35