
Flexible machining cell FPZ 250 Motor cooling unit
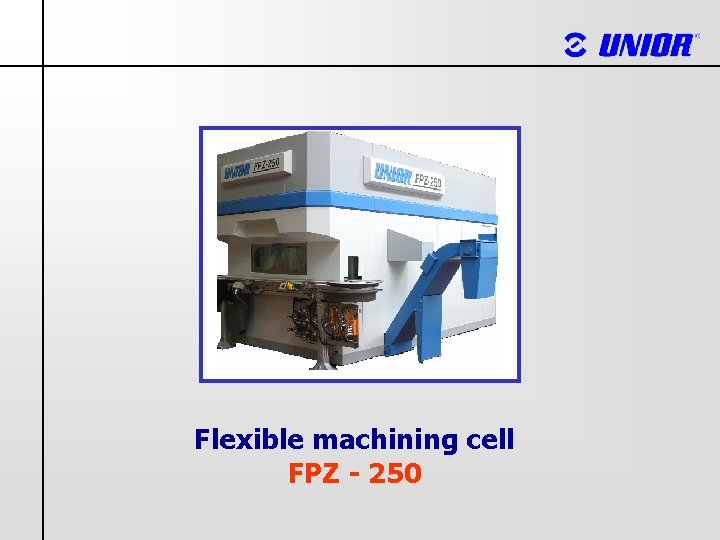
Flexible machining cell FPZ - 250
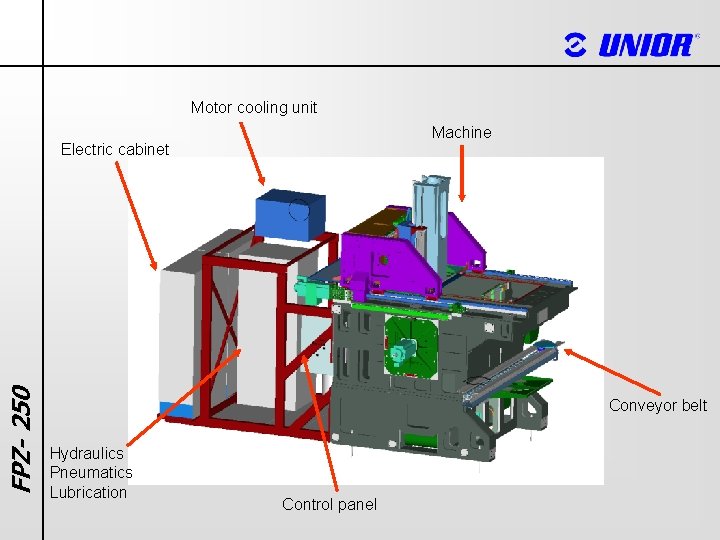
Motor cooling unit Machine FPZ- 250 Electric cabinet Conveyor belt Hydraulics Pneumatics Lubrication Control panel
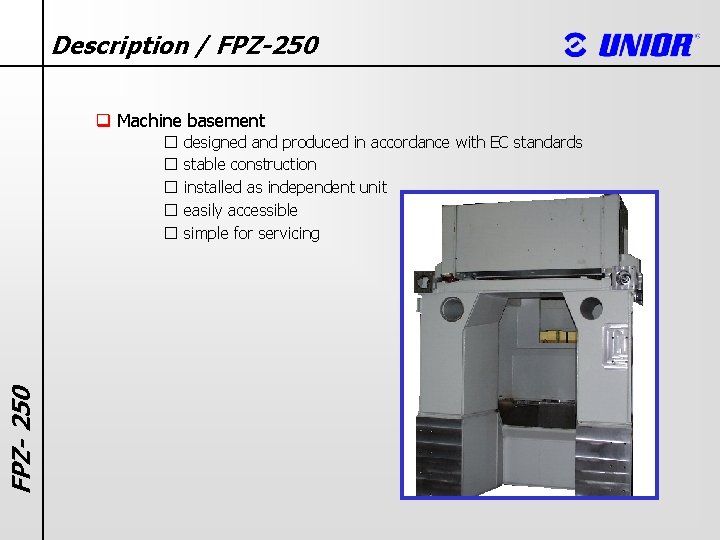
Description / FPZ-250 q Machine basement FPZ- 250 � � � designed and produced in accordance with EC standards stable construction installed as independent unit easily accessible simple for servicing

Description/ FPZ-250 q X-axis � � stroke 600 mm v = 60 m/min a = 6 m/s 2 measuring laths 5μm Heidenhain q Y-axis � � stroke 1200 mm v = 100 m/min a = 6 m/s 2, Option 10 m/s 2 measuring laths 5μm Heidenhain FPZ- 250 q Z-axis � � � stroke 600 mm v = 60 m/min a = 6 m/s 2 measuring laths 5μm Heidenhain pneumat. cylinder f. mass balancing
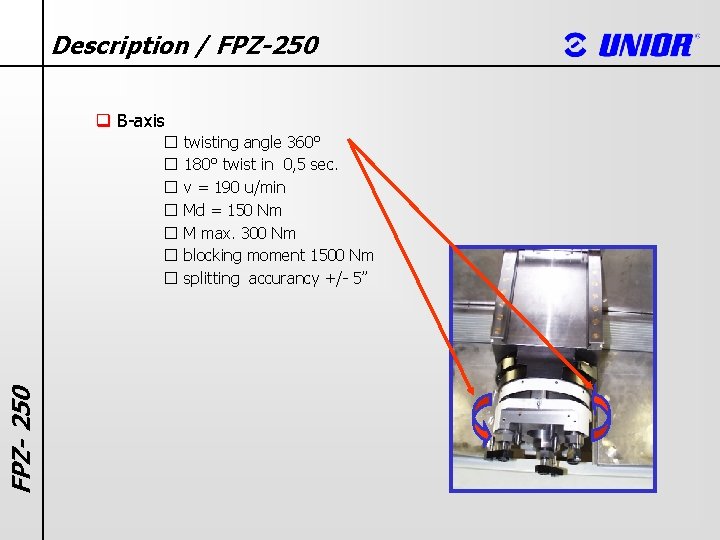
Description / FPZ-250 q B-axis FPZ- 250 � � � � twisting angle 360° 180° twist in 0, 5 sec. v = 190 u/min Md = 150 Nm M max. 300 Nm blocking moment 1500 Nm splitting accurancy +/- 5”
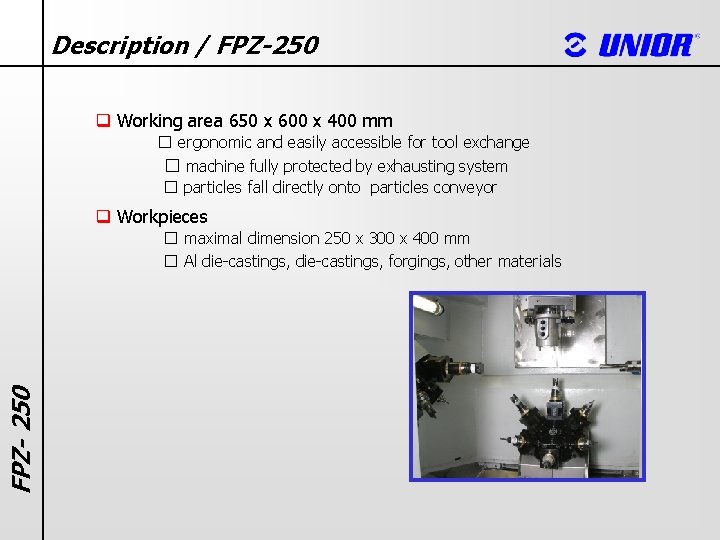
Description / FPZ-250 q Working area 650 x 600 x 400 mm � ergonomic and easily accessible for tool exchange � machine fully protected by exhausting system � particles fall directly onto particles conveyor q Workpieces FPZ- 250 � maximal dimension 250 x 300 x 400 mm � Al die-castings, forgings, other materials
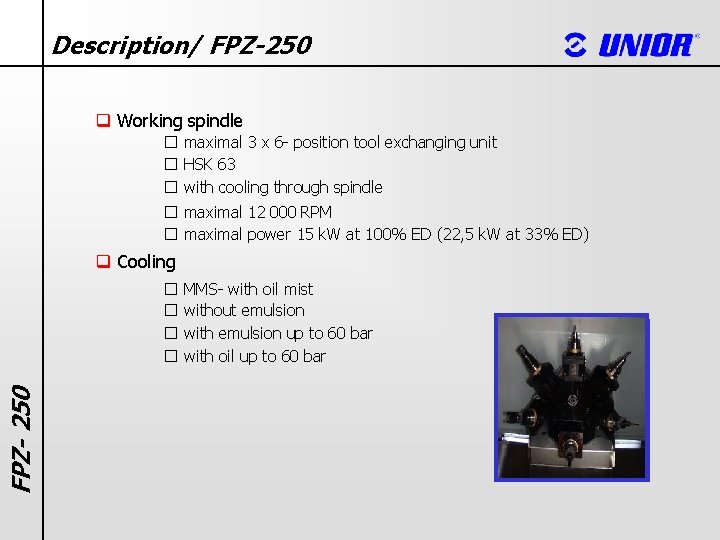
Description/ FPZ-250 q Working spindle � maximal 3 x 6 - position tool exchanging unit � HSK 63 � with cooling through spindle � maximal 12 000 RPM � maximal power 15 k. W at 100% ED (22, 5 k. W at 33% ED) q Cooling FPZ- 250 � � MMS- with oil mist without emulsion with emulsion up to 60 bar with oil up to 60 bar

Description / FPZ-250 q Jig clamping FPZ- 250 � � � HSK 100 with 4 brackets for orientation with 6 hydraulic connections 2 pneumatic connections for workpiece line-surface inspection 2 pneumatic connections for workpiece clamping inspection option for automated jig exchange
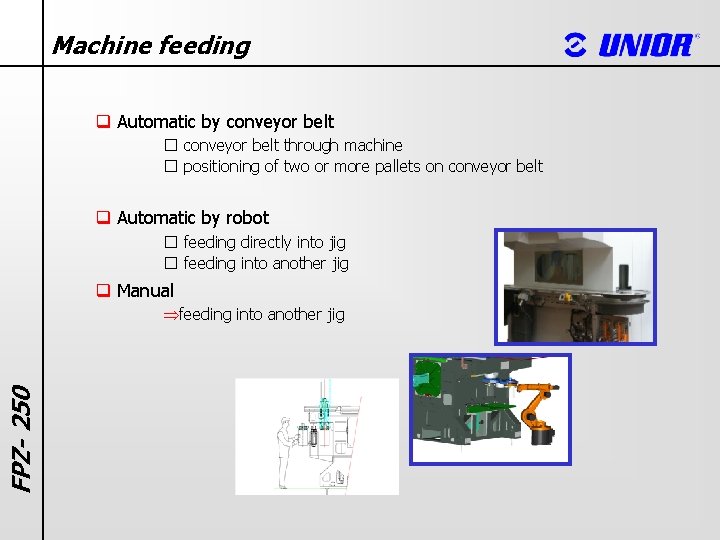
Machine feeding q Automatic by conveyor belt � conveyor belt through machine � positioning of two or more pallets on conveyor belt q Automatic by robot � feeding directly into jig � feeding into another jig q Manual FPZ- 250 Þfeeding into another jig
Secondary times q Time between two machining operations � less than 1 sec q Tooling exchange � at turret block < 2, 5 sec. � at tool exchanger < 1 sec. q Workpiece exchange FPZ- 250 � at pick-up system approx. 8 sec. � at pallet exchange approx. 6 sec.
Advantages in comparison with machining centres q Time between machining operations lower than 1 sec. q No problems with particles at machining in dry conditions (jig hanging) q Pick-up system of workpiece clamping � only one jig necessary � no need on separate feeding device and/or robot q Easy to connect into system q Machining from 5 sides possible FPZ- 250 q Simultaneous 4 -axis machining possible
Advantages-general q Spindle with workpiece jig vertical � pick-up system for rapid workpiece exchange q Accurrancy independent on � workpiece weight � jig weight � overhang ( Z-axis ) q Jig exchange FPZ- 250 � connection by six hydraulic rings � connection by two pneumatic rings – line –surface inspection � clamping through pallet possible q Simple accessibility to all tools q Constructed compact as uniform whole � no need for disassembling during transport � short start-up time at site of installation

Tool exchanging unit ( 20 / 30 tools ) Turret block (up to 6 tools or smaller multi -spindle head ) Multi-spindle heads (nunber of spindles according to requirements )
- Slides: 13